CNC-turned contact pins and terminals
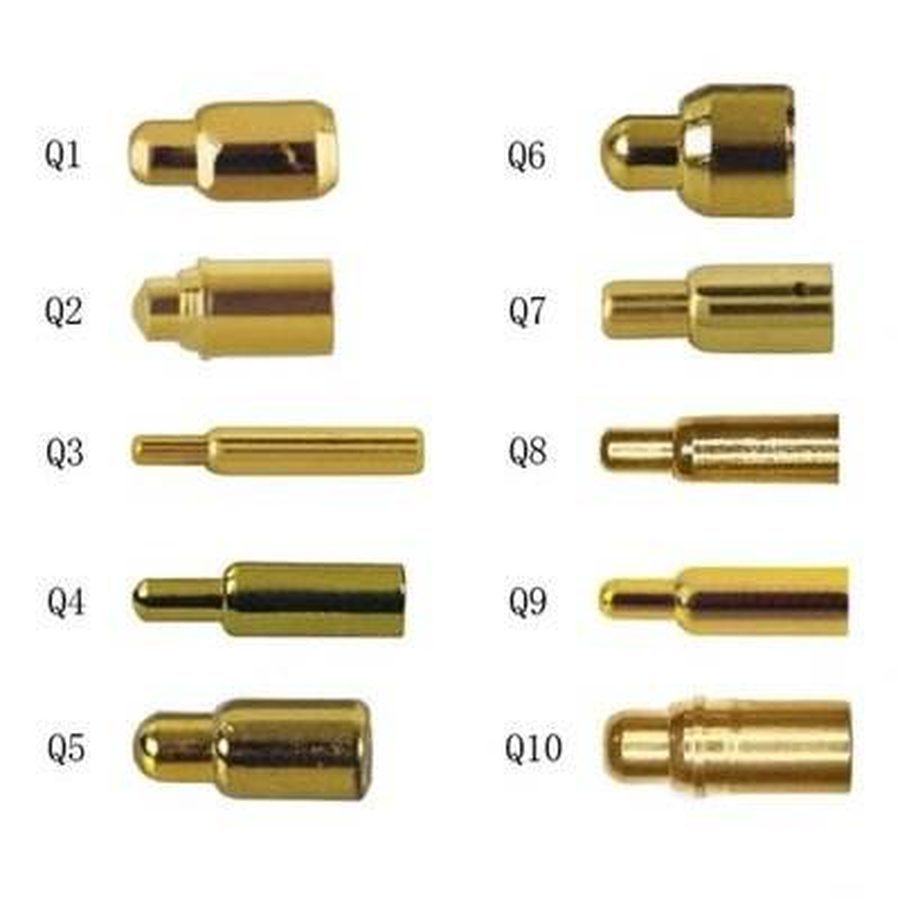
Small turned and milled contacts — pogo pins, terminals and spacers — machined to the same ±0.01 mm the toolroom works to.
Products · Metal parts
Rings, collars and spacer sets milled and turned from stainless steel and aluminium, with bores and faces held to a common datum.
Also searched asCNC machining China · turned parts · machined stainless parts · stamping die maker · custom metal parts supplier
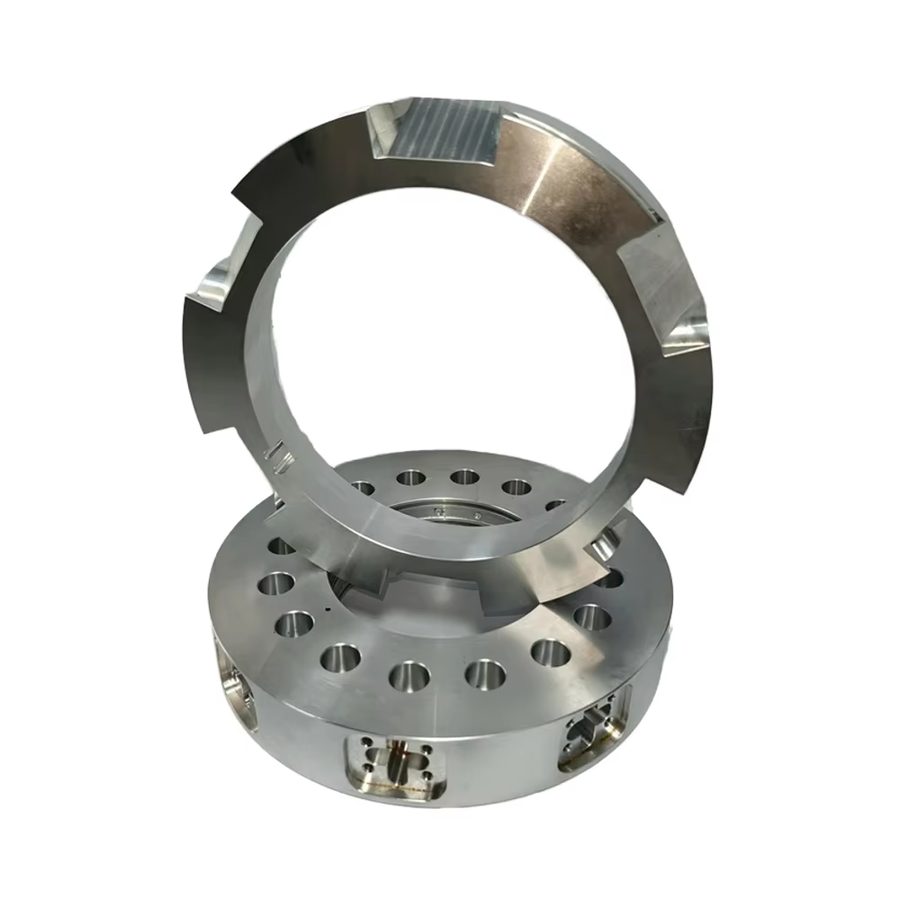
A ring is judged by two things: whether the bore and the flange stay concentric, and whether the two faces stay parallel after clamping. Both are machining decisions, so the part is roughed, stress-relieved where the wall is thin, and finished in a single setup on a 0.001 mm CNC centre where the geometry allows it.
These parts suit fixtures, sensor housings, collars and clamp sets that sit inside an assembly rather than on show. We work from your STEP file and agree the datum scheme and the inspection points in the DFM review, so the CMM report at first article measures the features you actually assemble against.
Specification
The same machines, the same inspection room and the same drawing discipline as the tooling side of the plant.
| Processes | CNC turning, CNC milling, drilling and tapping; wire-cut and EDM for die work |
| Materials | Aluminium, stainless steel, brass and copper alloys, titanium |
| Machine accuracy | Down to 0.001 mm (Yasoda, OKUMA, GF, Makino) |
| Part tolerance | ±0.01 mm on critical features, agreed on the drawing |
| Surface | As machined, bead-blasted or polished; plating and anodising to your spec |
| Inspection | First article on the Swiss Hexagon CMM, with a dimensional report |
| Batch size | Prototype quantities through to production runs |
| Documentation | 2D/3D drawings, material certificate, inspection report |
Values above are our standard capability for this class of part, not fixed figures for a specific job. Material, finish and the inspection plan are agreed on the drawing before a bar is cut.
Related products · Metal Parts
Small turned and milled contacts — pogo pins, terminals and spacers — machined to the same ±0.01 mm the toolroom works to.
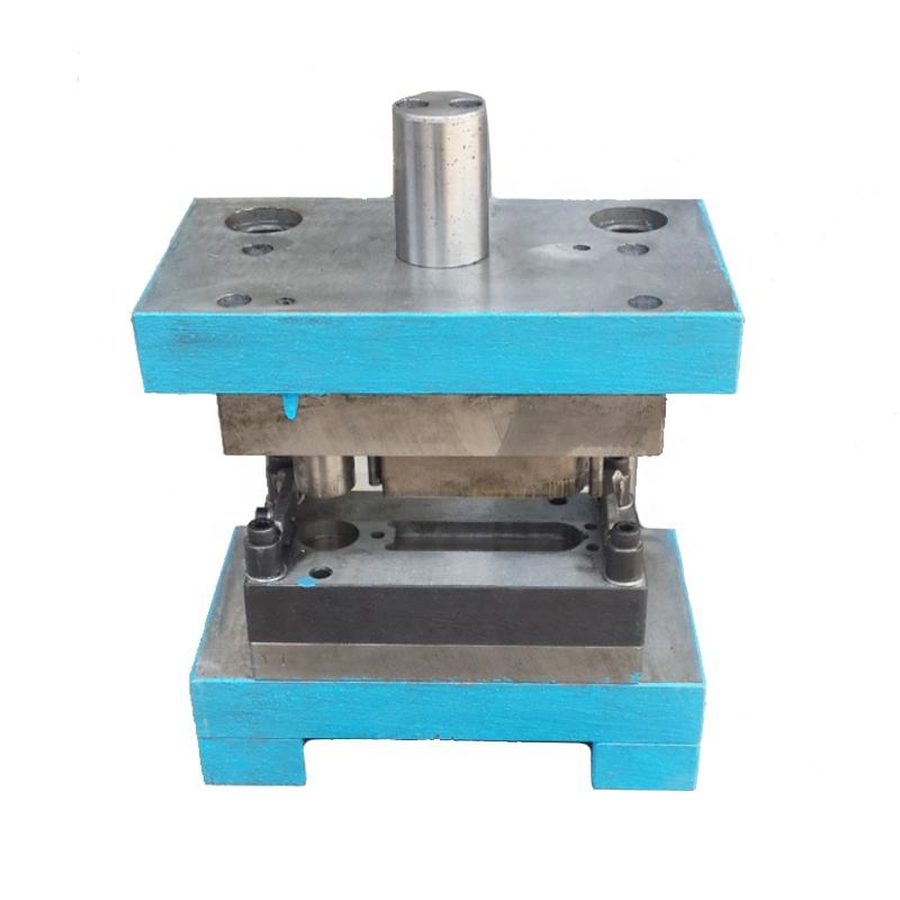
A single-station stamping die for tinplate boxes and shallow drawn panels — built, tried and corrected in the same toolroom as our injection molds.
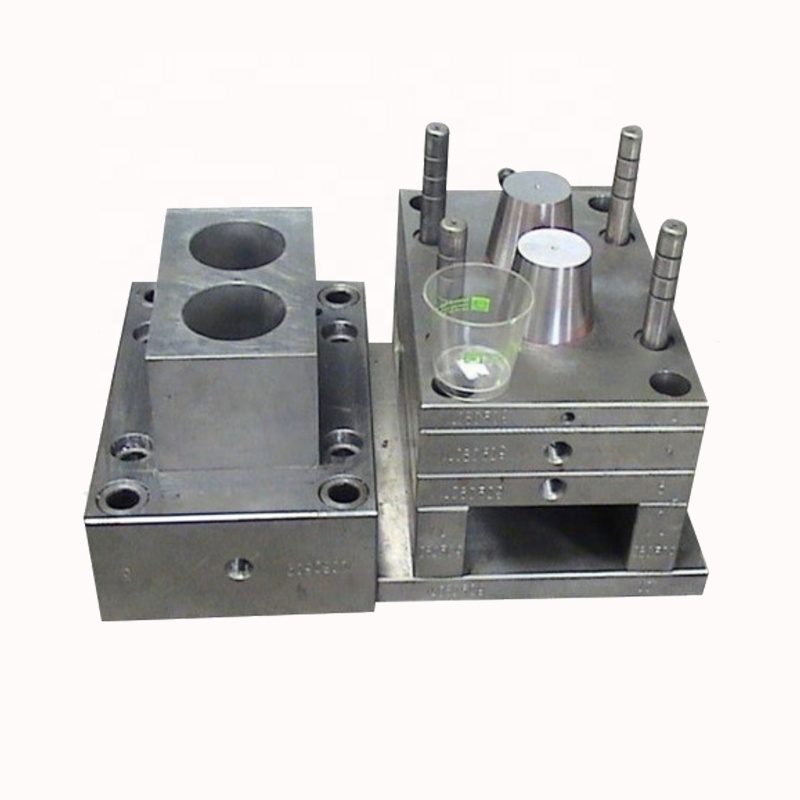
A compact two-cavity tool for cups and containers, with balanced cooling and a polished cavity finish for a clean visible surface.
Next step
STEP/IGES/X_T files, the resin, your annual volume and target market are enough to get a mold price, a cycle estimate and the risks we can see — usually in 1–2 business days.