CNC-turned contact pins and terminals
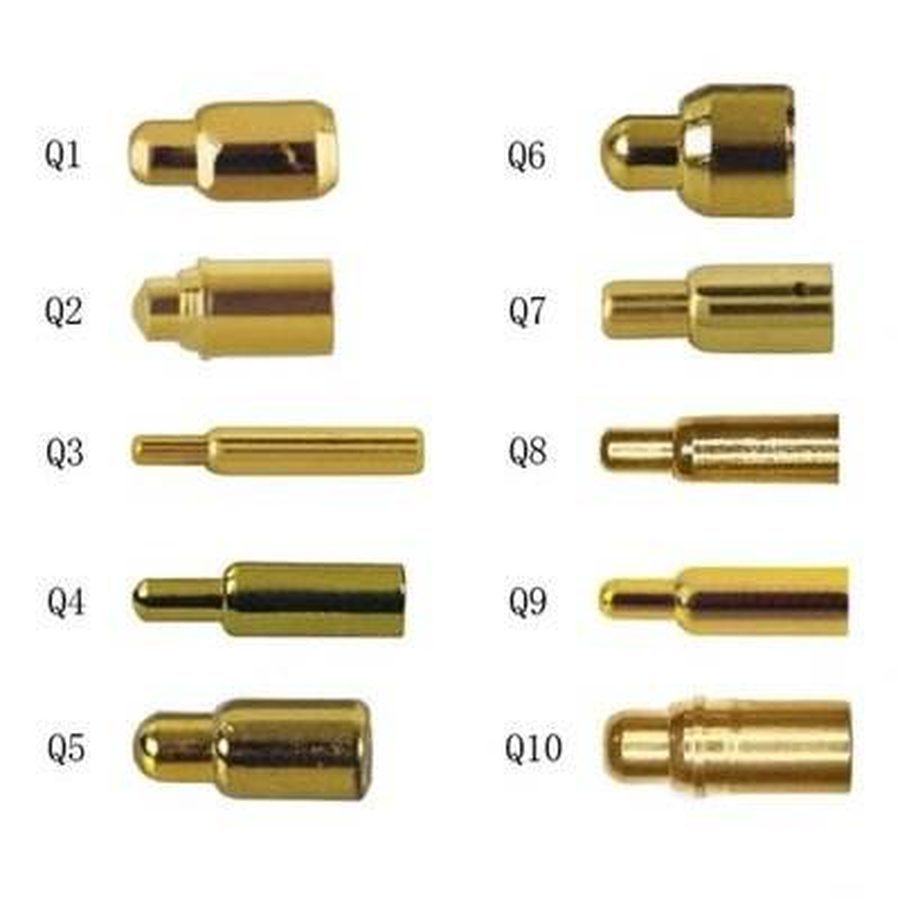
Small turned and milled contacts — pogo pins, terminals and spacers — machined to the same ±0.01 mm the toolroom works to.
Products · Metal parts
A single-station stamping die for tinplate boxes and shallow drawn panels — built, tried and corrected in the same toolroom as our injection molds.
Also searched asCNC machining China · turned parts · machined stainless parts · stamping die maker · custom metal parts supplier
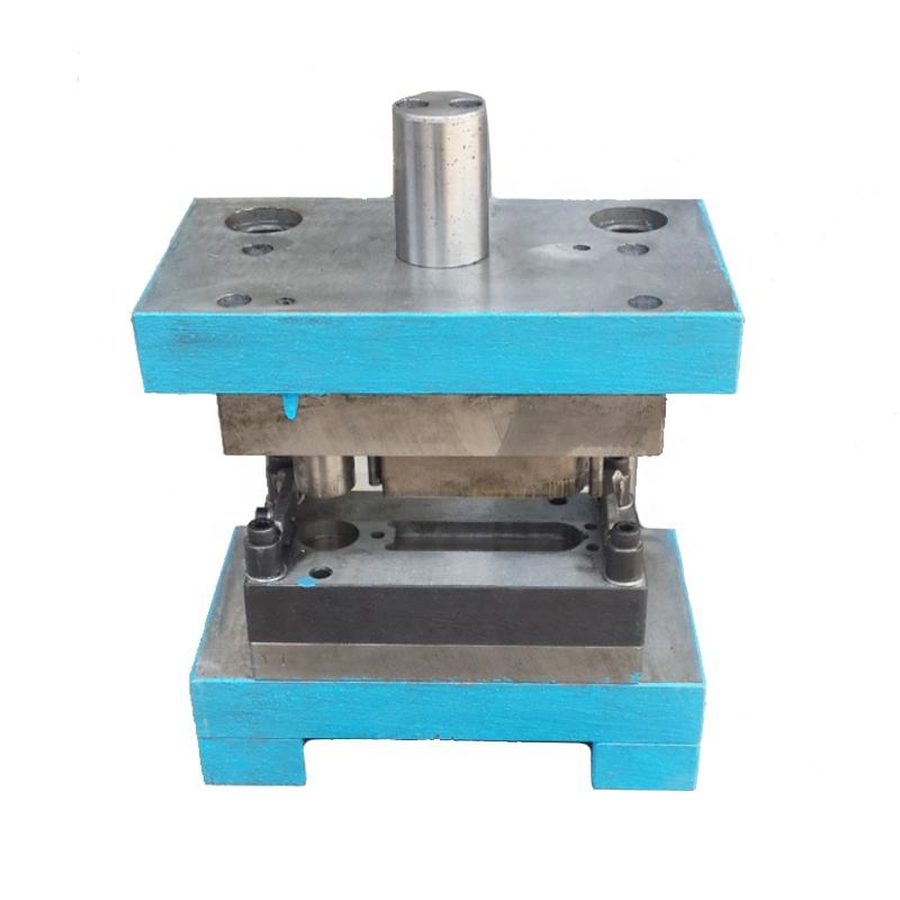
Not every tool in the shop is an injection mold. Tin boxes, shallow covers and punched brackets need a stamping die, and the toolroom skills are the same: plate machining at ±0.01 mm, wire-cut and sinker EDM for the punch and die clearance, and a guided punch assembly that stays aligned over a long run.
The die in the photograph is a single-station tool with a blue painted base, guide pillars and a stripper plate. We build the die, run the first parts on site and correct the clearance and the blank development before shipment, so you receive a tool that has already produced a sample you can measure.
Specification
The same machines, the same inspection room and the same drawing discipline as the tooling side of the plant.
| Processes | CNC turning, CNC milling, drilling and tapping; wire-cut and EDM for die work |
| Materials | Aluminium, stainless steel, brass and copper alloys, titanium |
| Machine accuracy | Down to 0.001 mm (Yasoda, OKUMA, GF, Makino) |
| Part tolerance | ±0.01 mm on critical features, agreed on the drawing |
| Surface | As machined, bead-blasted or polished; plating and anodising to your spec |
| Inspection | First article on the Swiss Hexagon CMM, with a dimensional report |
| Batch size | Prototype quantities through to production runs |
| Documentation | 2D/3D drawings, material certificate, inspection report |
Values above are our standard capability for this class of part, not fixed figures for a specific job. Material, finish and the inspection plan are agreed on the drawing before a bar is cut.
Related products · Metal Parts
Small turned and milled contacts — pogo pins, terminals and spacers — machined to the same ±0.01 mm the toolroom works to.
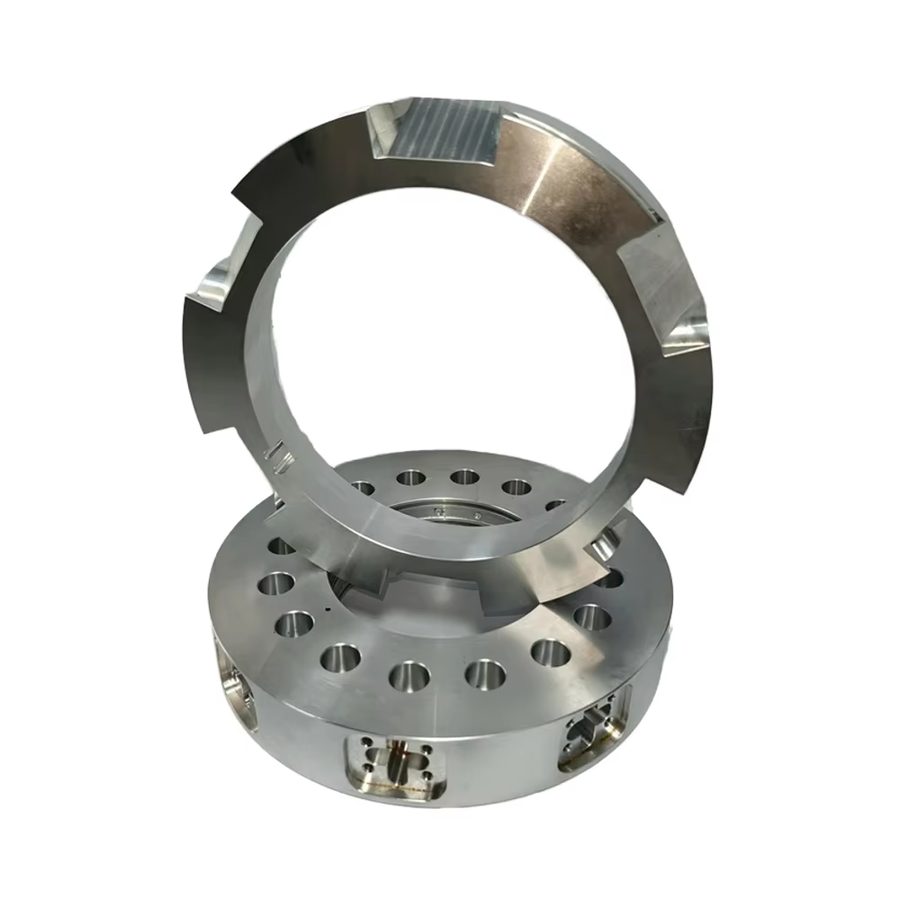
Rings, collars and spacer sets milled and turned from stainless steel and aluminium, with bores and faces held to a common datum.
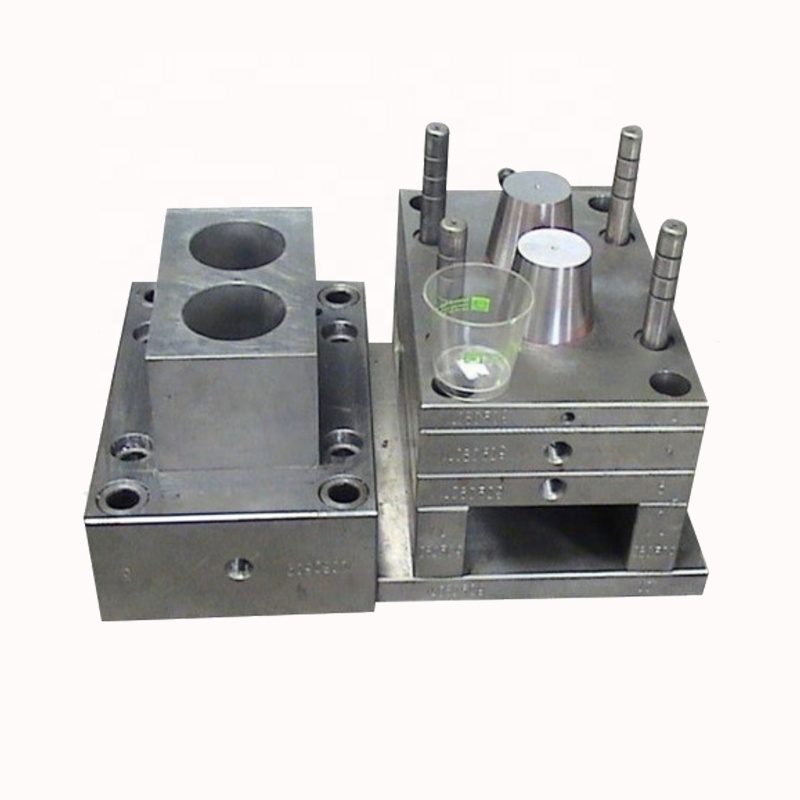
A compact two-cavity tool for cups and containers, with balanced cooling and a polished cavity finish for a clean visible surface.
Next step
STEP/IGES/X_T files, the resin, your annual volume and target market are enough to get a mold price, a cycle estimate and the risks we can see — usually in 1–2 business days.