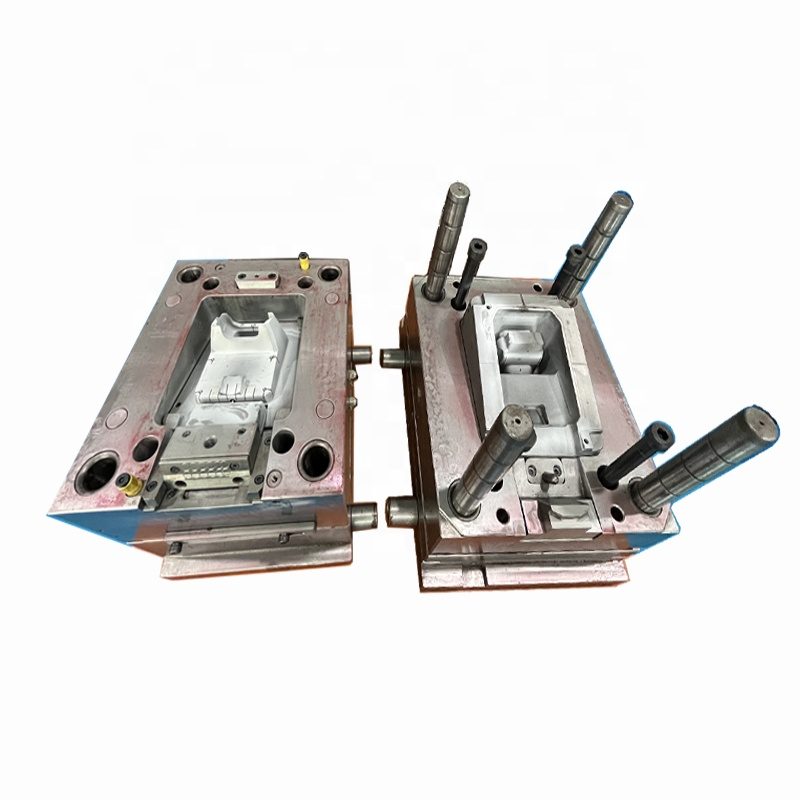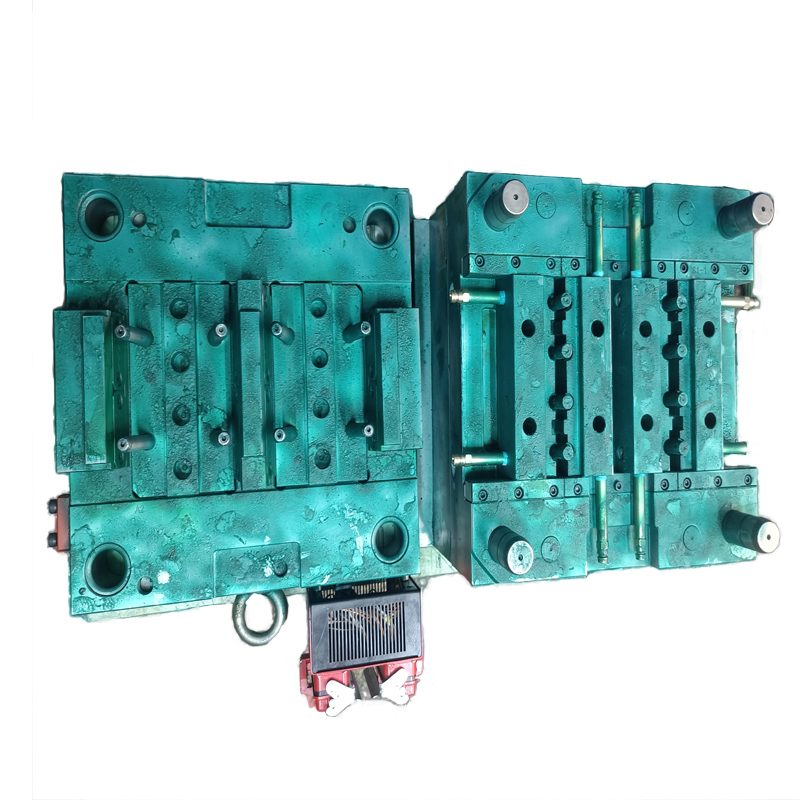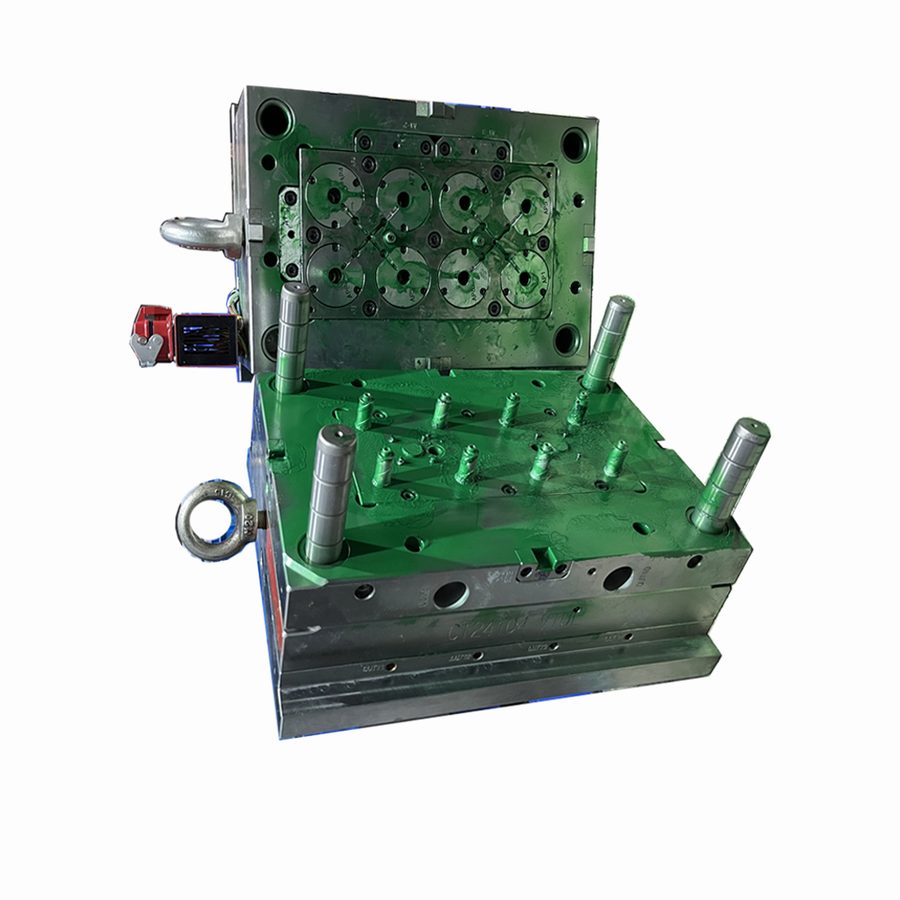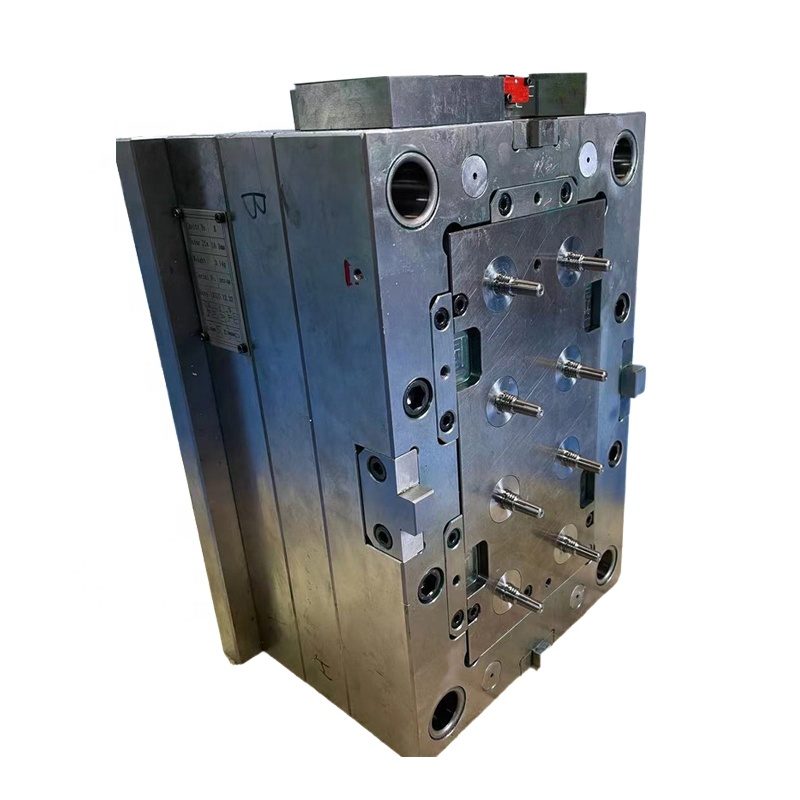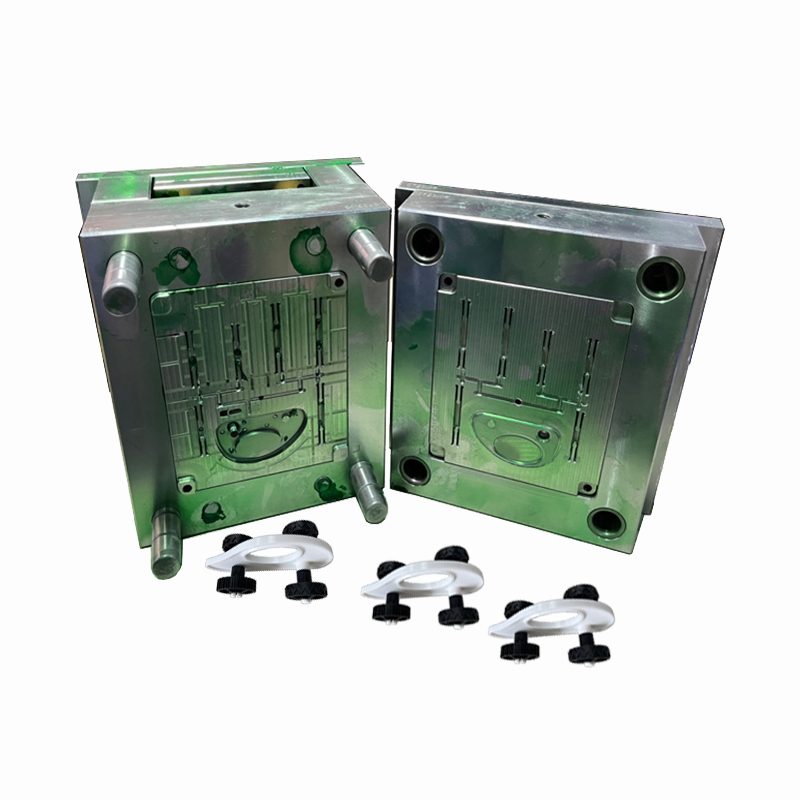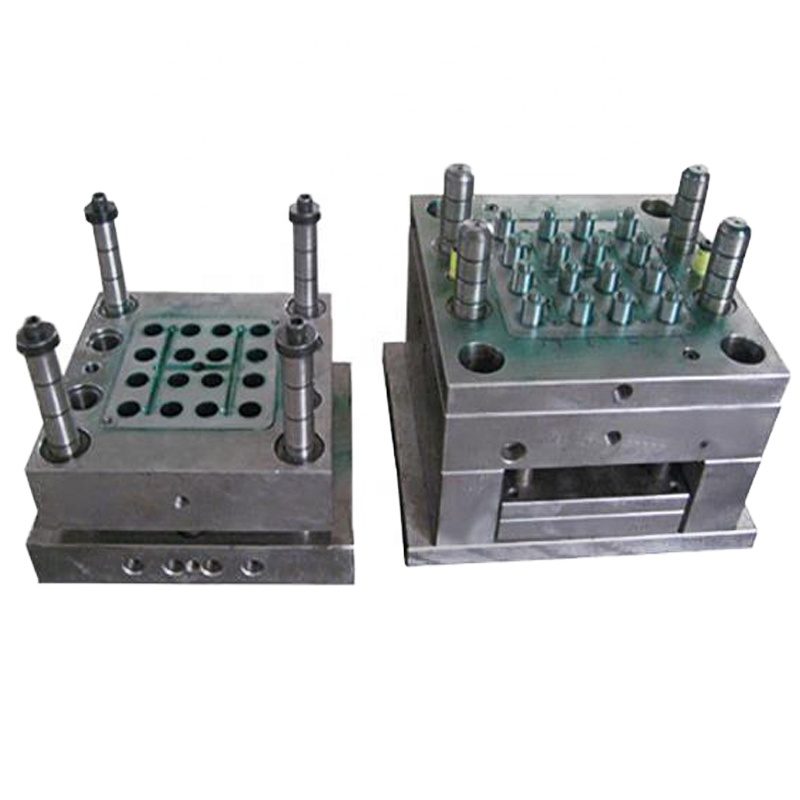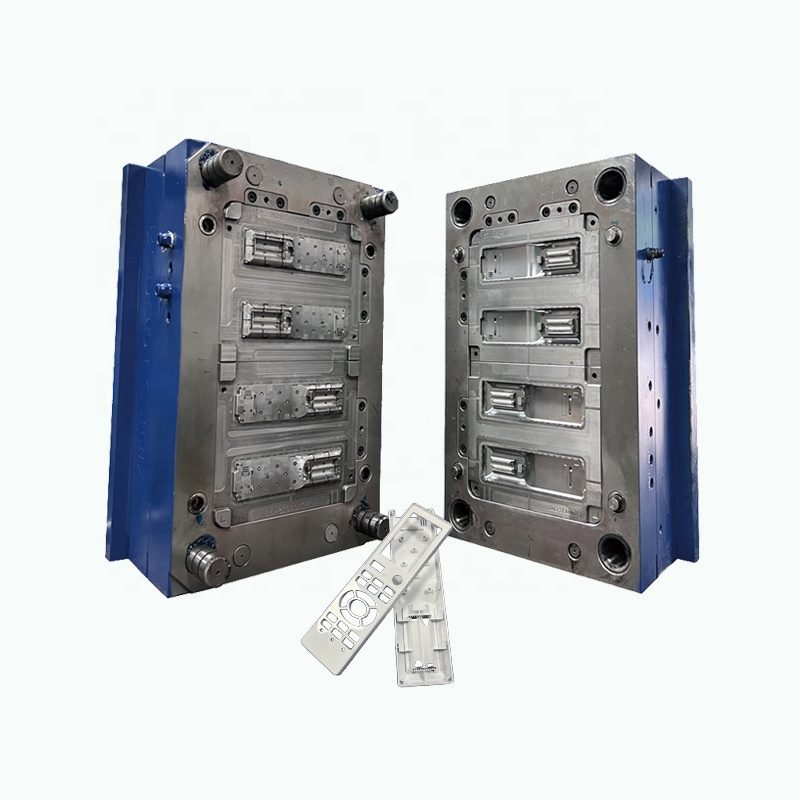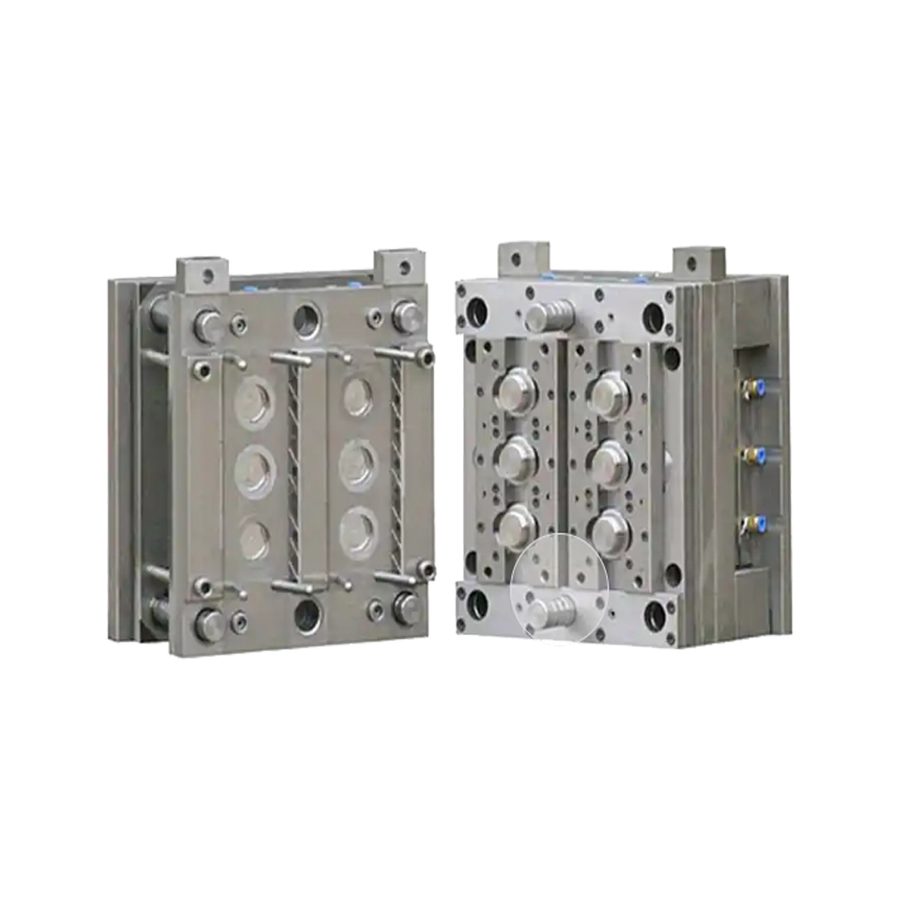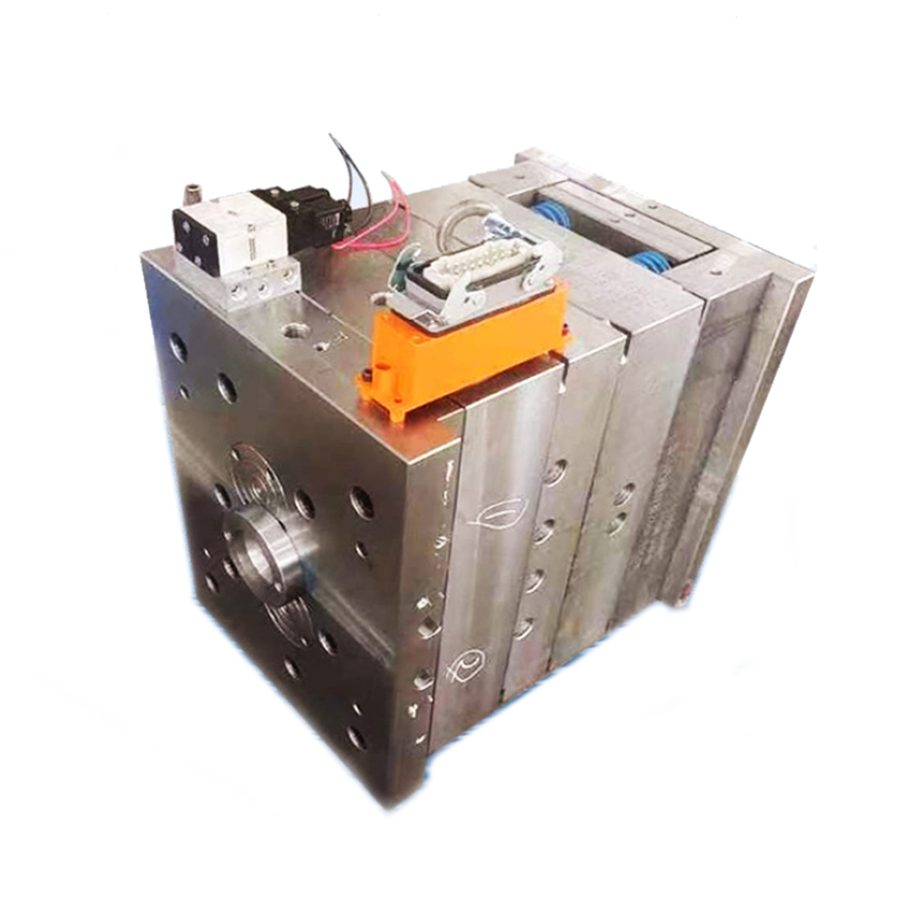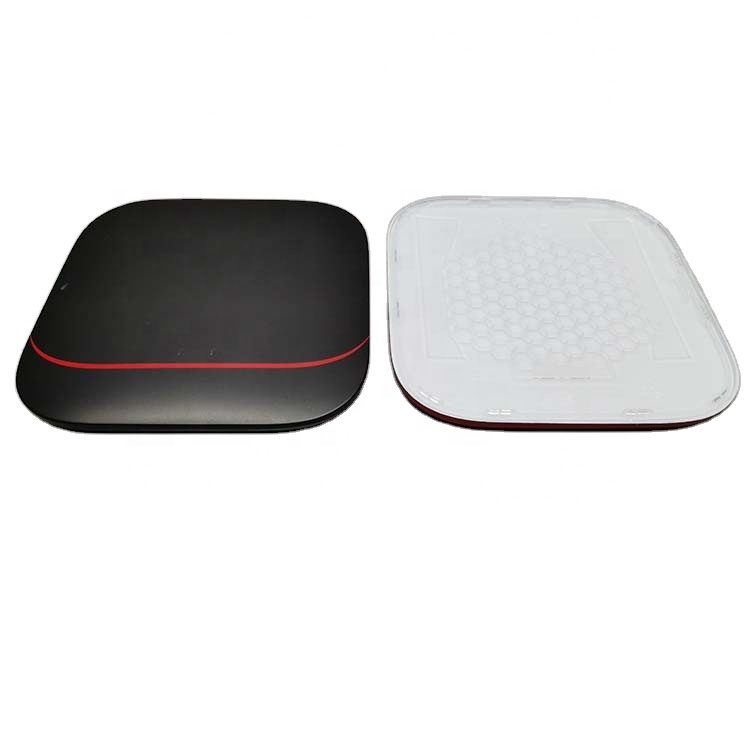
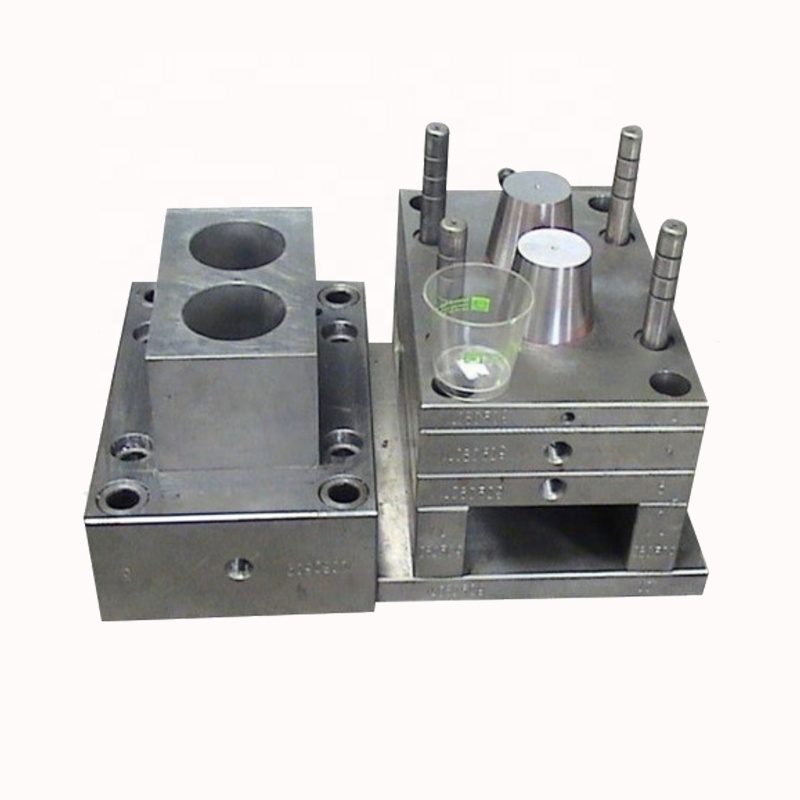
Two-cavity container mold
A compact two-cavity tool for cups and containers, with balanced cooling and a polished cavity finish for a clean visible surface.
Products
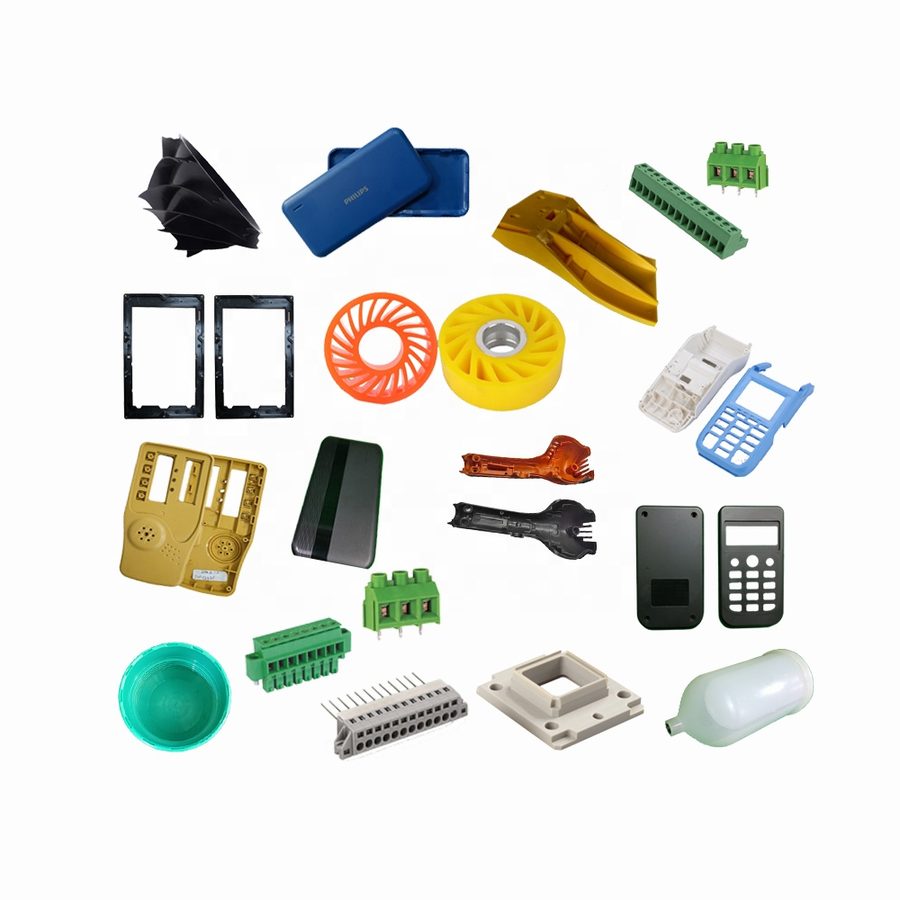
42 tooling and part examples from our own plant in Humen, Dongguan. Five ranges, one factory: injection moulds and tooling we designed, machined, polished and trialled; overmolded parts that put two materials in one component; IMD / IML parts decorated in the mould rather than after it; metal parts cut on the same machines; and the precision injection parts produced on our own 30 presses. Every tool is engineered and quoted to your part rather than sold from a shelf.
CENTS builds custom injection molds for plastic parts — from single-cavity prototype tools to multi-cavity production molds with hot runners, slides, unscrewing cores and collapsible cores — and molds the parts in the same building on 30 presses from 20T to 300T. Mold work is held to ±0.01 mm and verified on a Swiss Hexagon CMM. The catalogue is arranged in five ranges: injection moulds, overmolding parts, IMD / IML parts, metal parts and precision injection parts. Send 3D data, resin and annual volume for a price, a cycle estimate and a written DFM report.
Category 01 · Injection moulds
Two-plate and three-plate tools, multi-cavity grids, insert and family molds, slide and unscrewing mechanisms, and cosmetic-grade polished cavities. Written in the spelling and the vocabulary your engineers search with — mold or mould, tooling or toolmaking.
What buyers type when they search this range
A compact two-cavity tool for cups and containers, with balanced cooling and a polished cavity finish for a clean visible surface.
A two-plate production mold with mirror-polished cavity and core plates, built for visible Class-A surfaces.
Undercuts solved with cam-driven slides rather than a redesign — for parts with side holes, clips, snap hooks or external features.
High-cavitation tooling with replaceable cores in a common mold base — output per cycle without rebuilding the whole tool.
Mold base plates, cavity blocks and inserts machined, ground and fitted in-house — the hidden half of mold quality.
Several different parts of one product in a single tool — the economical route when volumes per part are low but the assembly needs all of them.
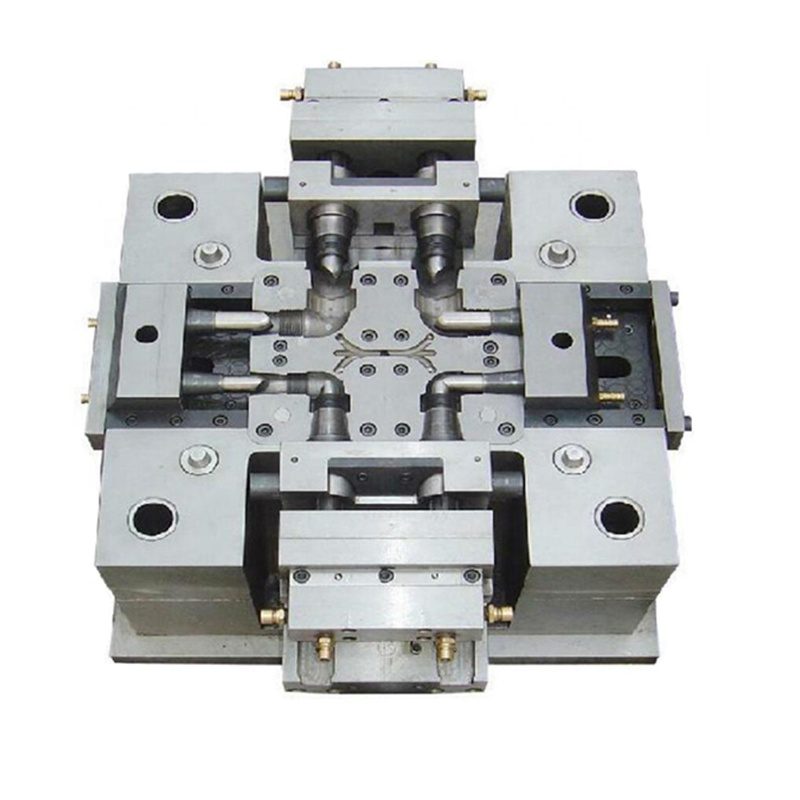
Complex tooling for pipe fittings, connectors and technical components where several undercuts and cores must sequence correctly.
Surface finishing as an engineered step: hand polishing to SPI classes and texturing for grip, gloss control and brand look.
Cap tooling with a mirror-grade cavity, controlled fit and multi-cavity layout for packaging that is handled every day.
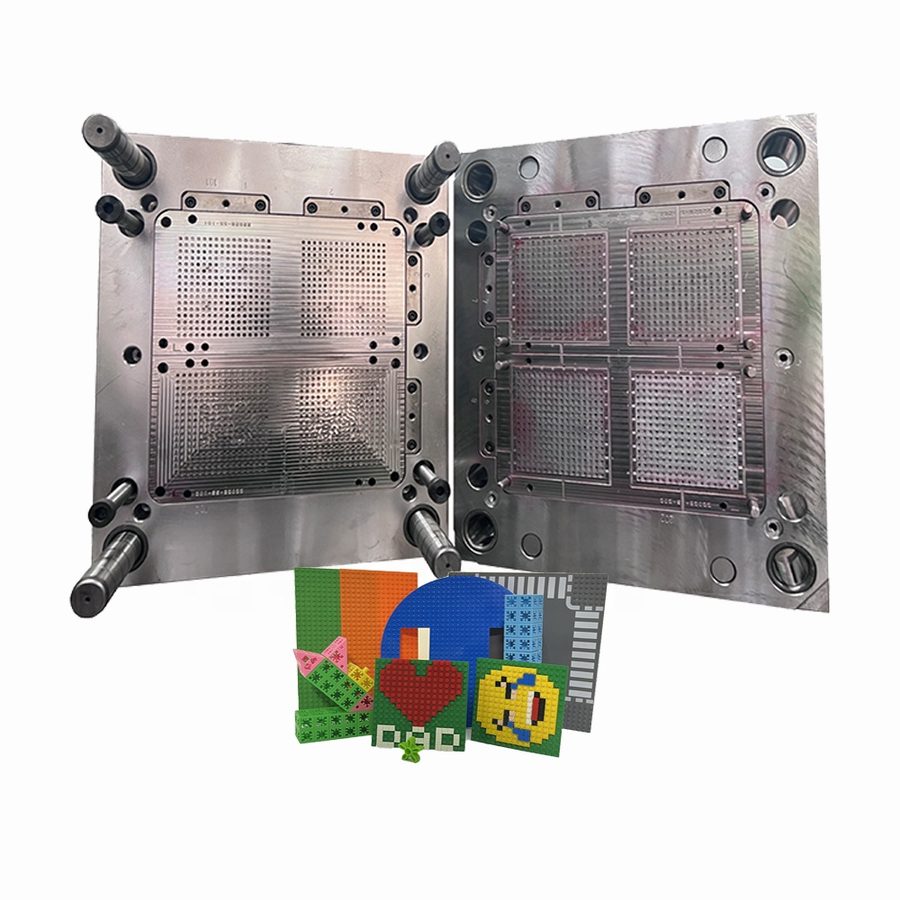
Many small cavities in a hardened tool, laid out for balanced fill and economical high-volume production of one part.
Segmented insert construction with engineered venting — for parts that trap gas or need individually replaceable cavity detail.
Modular cavity inserts in a common frame — engineered so revisions and maintenance touch one insert, not the whole tool.
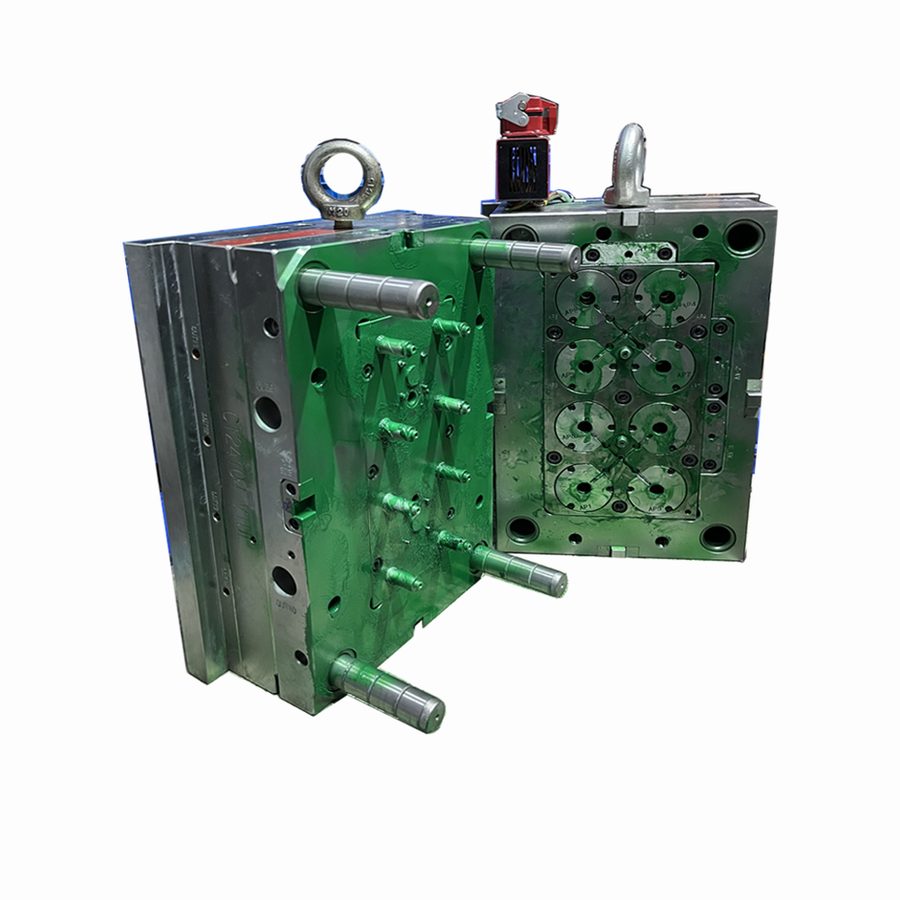
Larger tooling engineered for press handling, lift points and mechanical side action rather than for the bench.
Category 02 · Overmolding parts
Two materials in one component: a rigid substrate with a soft TPE, TPU or silicone skin bonded during molding, or a metal insert encapsulated by the plastic. One part, no assembly step, no adhesive.
What buyers type when they search this range
The bond is the engineering: material pair, substrate pre-treatment, wall thickness over the insert and mold temperature at the interface are agreed in the DFM review, not discovered at T1.
A rigid moulding with a soft silicone element bonded in place — two materials, one component, no assembly step.
Category 03 · IMD / IML parts
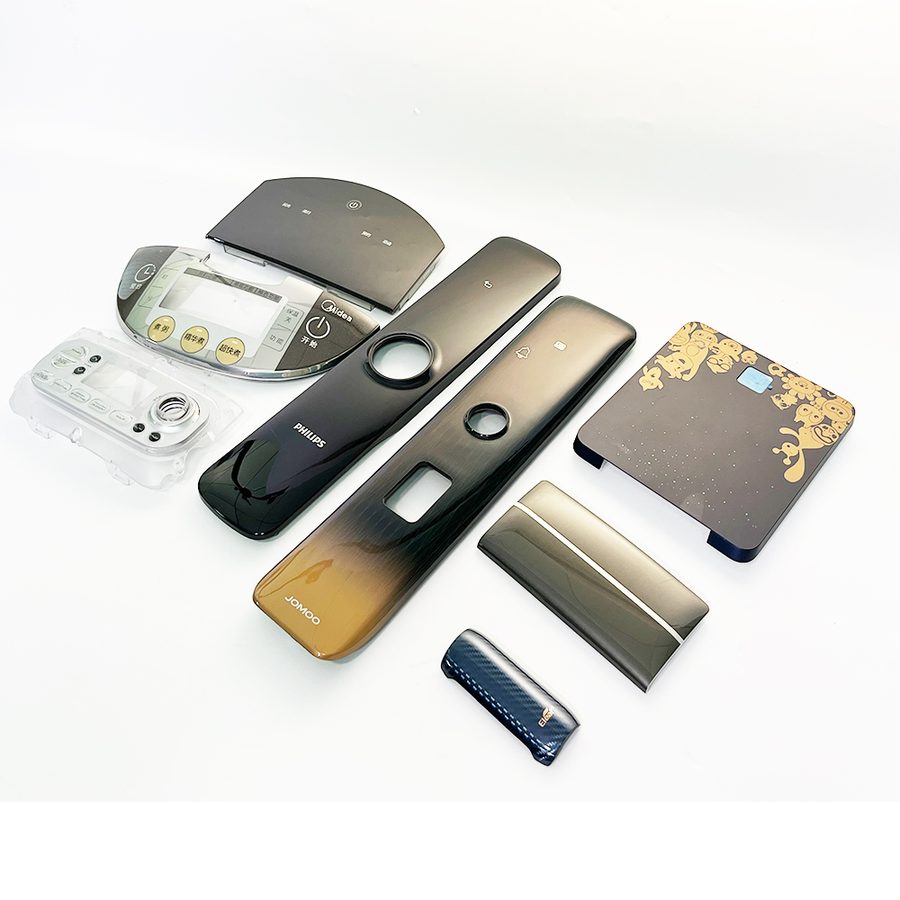
Decoration bonded into the molding rather than printed on top: film insert and label graphics, backlit panels, hard-coated lenses and metallic or gradient finishes that survive handling, cleaning and abrasion.
What buyers type when they search this range
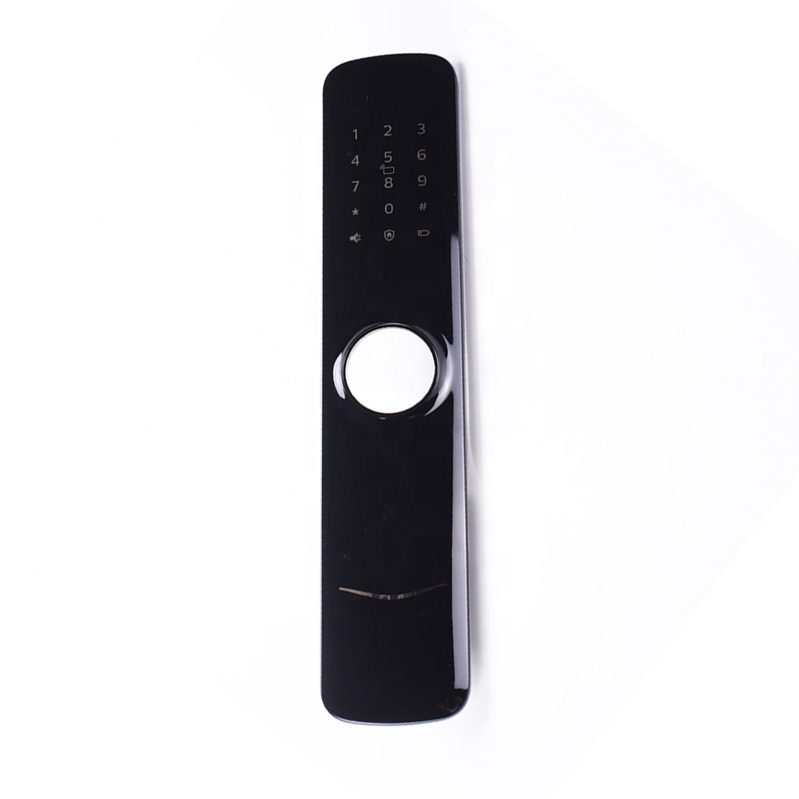
A slim decorated control panel for smart locks — graphics in the mold, so the finish does not wear off in daily use.
Flat decorated panels with metallic, gradient and marble finishes — produced as flat parts instead of printed foil or metal.
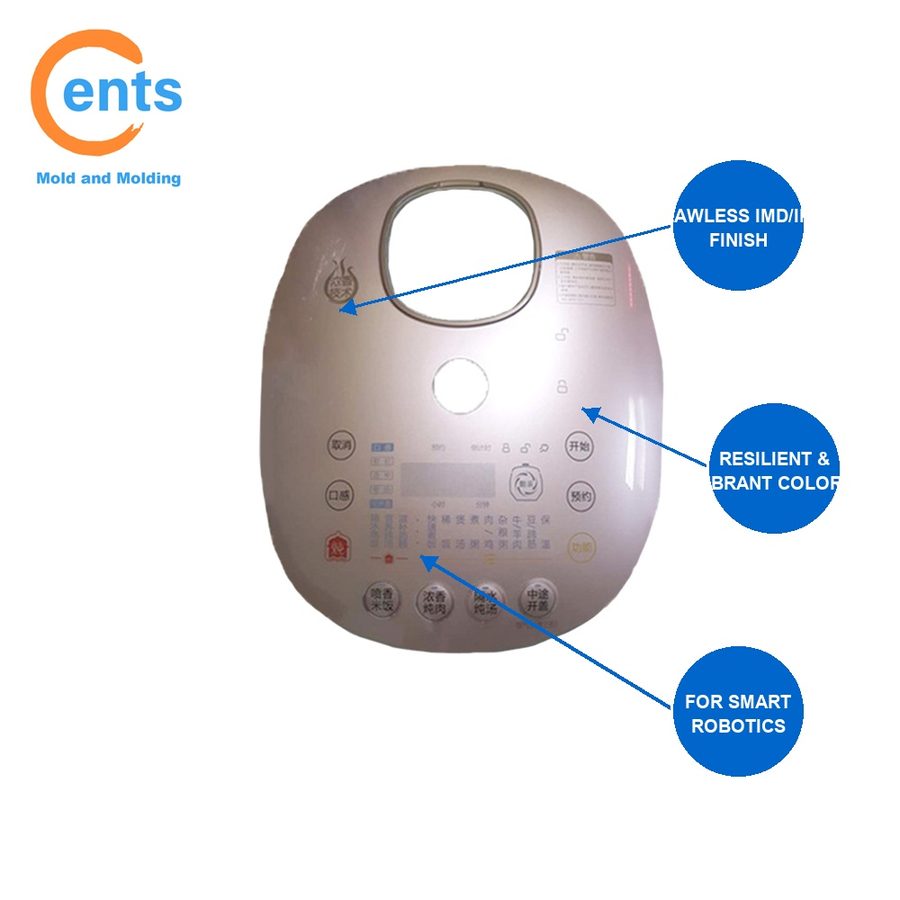
A molded shell where colour and graphics sit inside the wall — seamless finish, brilliant colours and no post-printing.
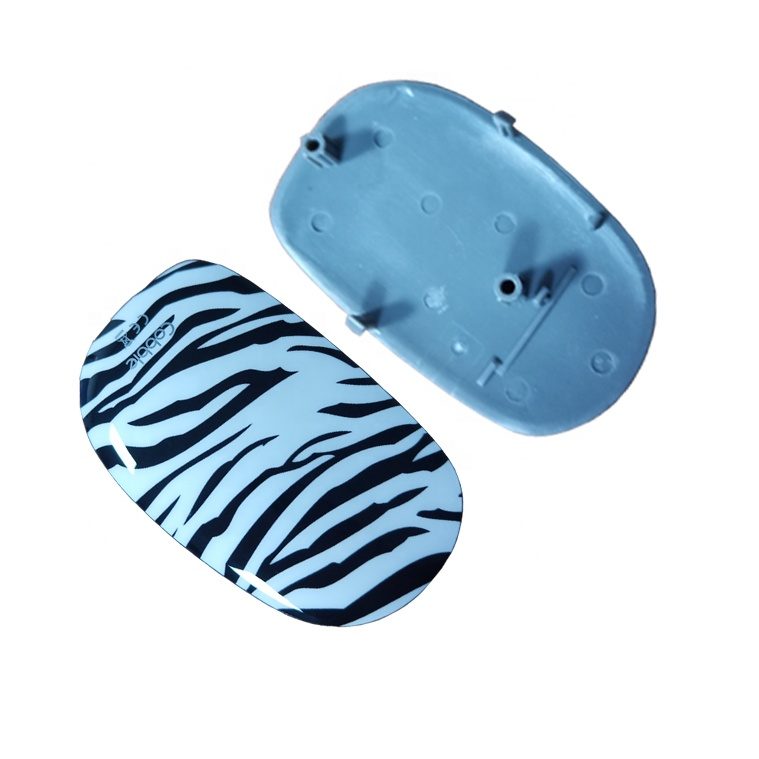
Printed patterns — animal print, textile effects, gradients — molded into small plastic parts instead of applied afterwards.
Two-part appliance housings with a class-A gloss surface and a mechanical clamshell fit.
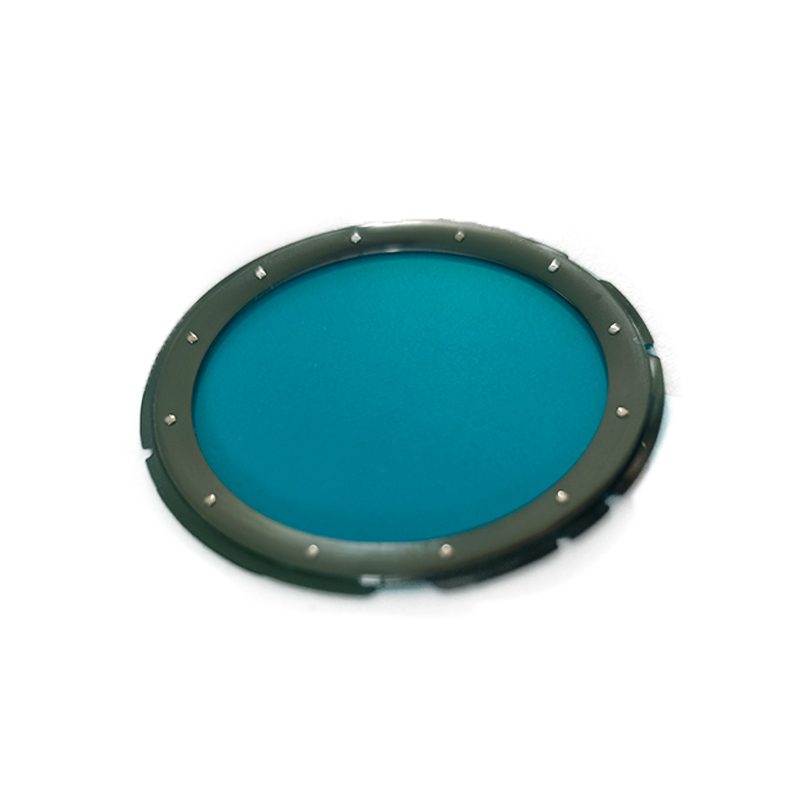
Gradient and depth-effect decoration molded into a curved cover — the look of a coated lens without the coating.
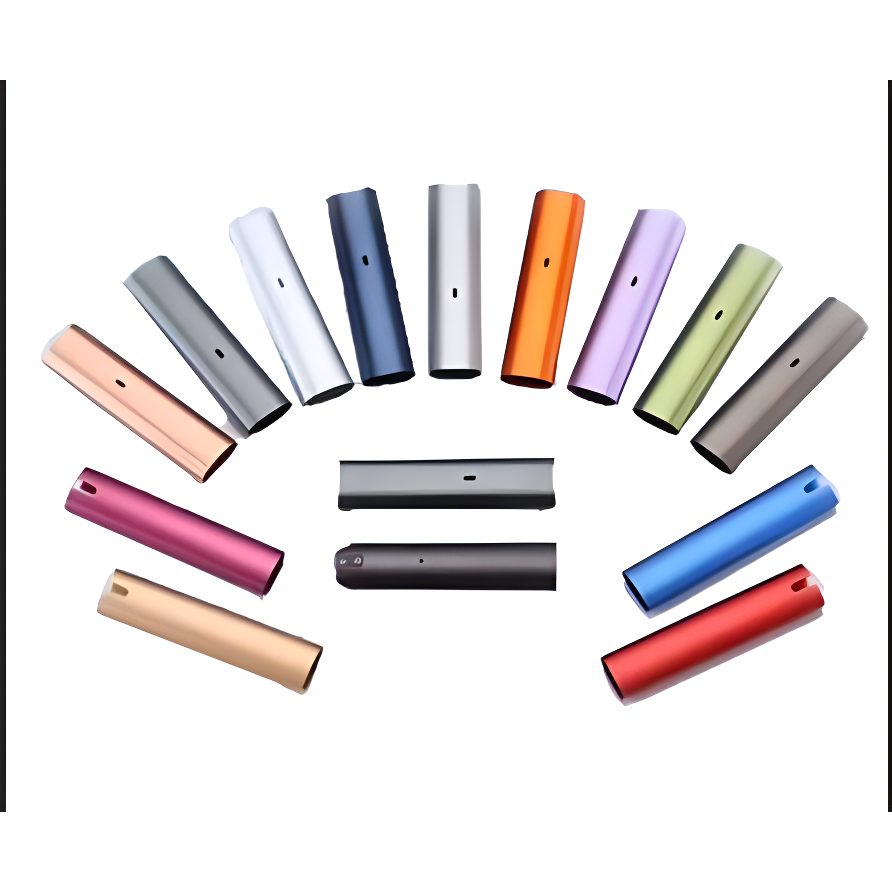
One tool, many colourways — the economical way to offer a product range without a mold per variant.
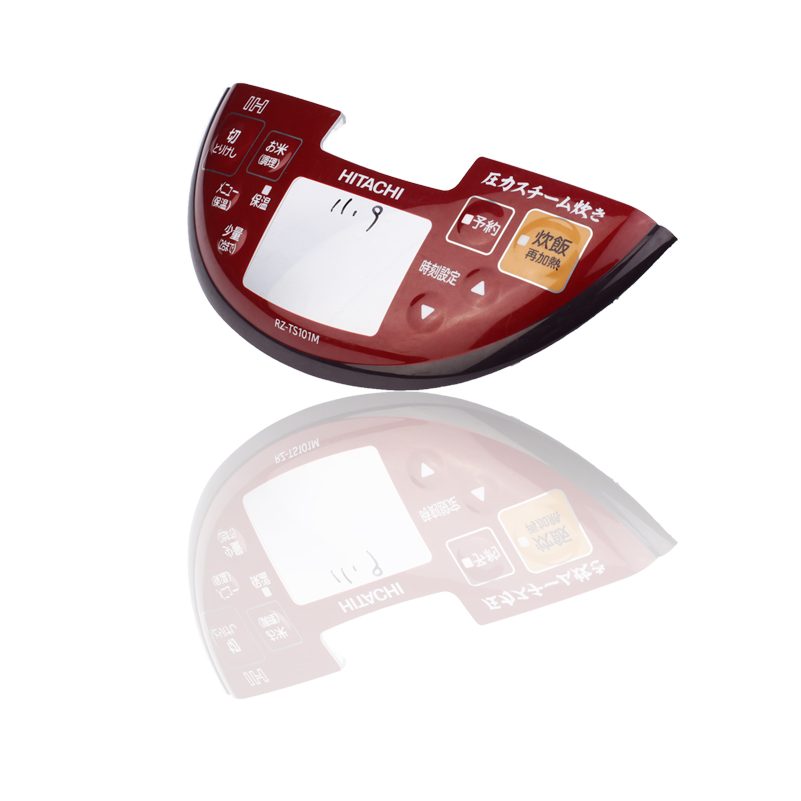
High-resolution artwork molded into a panel for appliances and consumer products — durable under repeated cleaning.
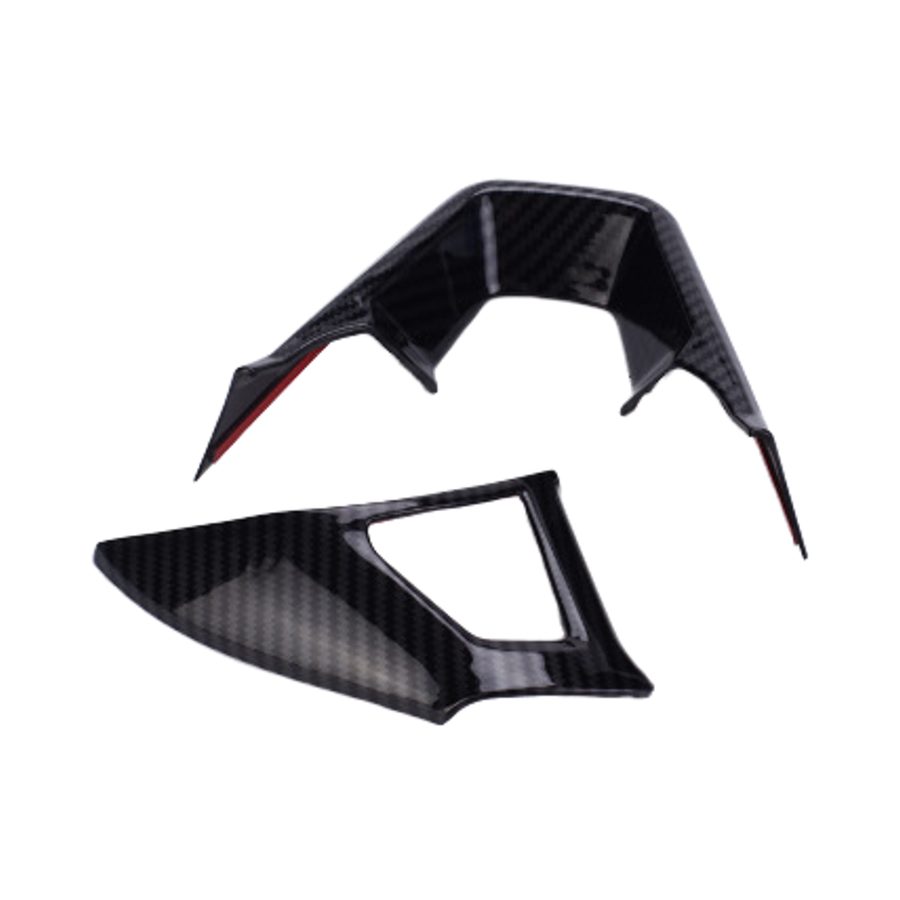
Carbon-weave and metallic trim for vehicle interiors — molded, not wrapped.
Small shells with hard-wearing in-mold labelling and a precise button aperture — the detail that decides perceived quality.
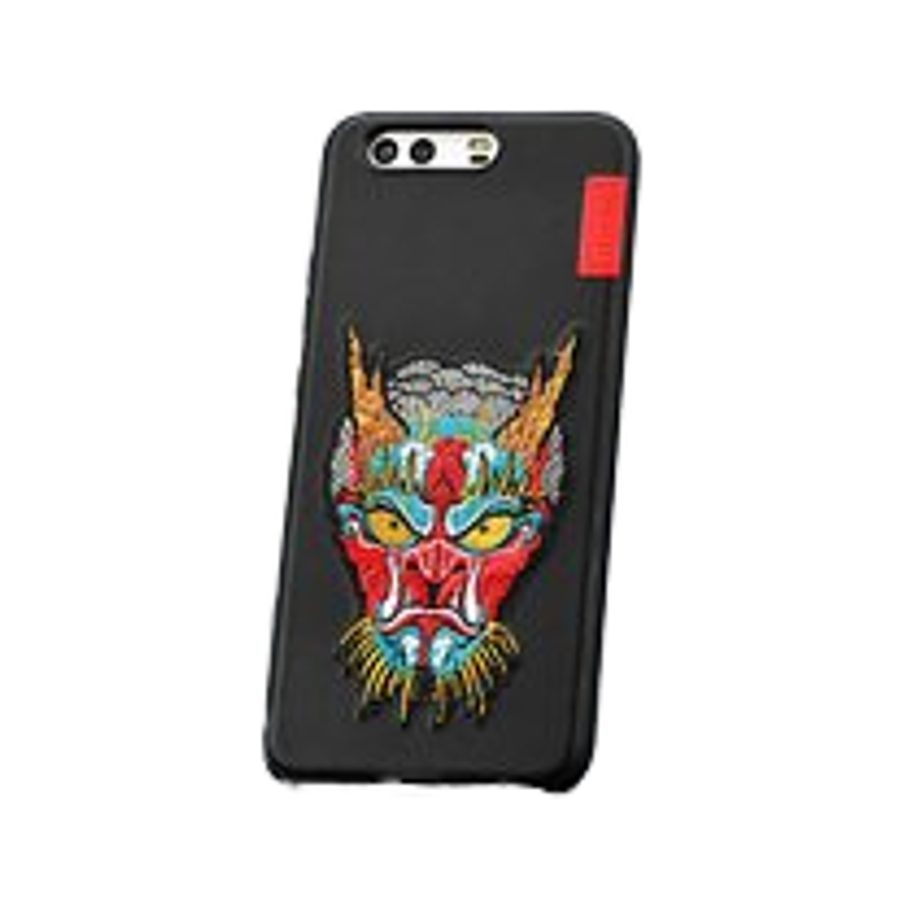
Slim protective cases with full-wrap printed graphics produced in-mold, not by pad printing.
Category 04 · Metal parts
The metal side of the same workshop: CNC-turned contacts, machined stainless rings and spacers, and sheet-metal stamping dies for tinplate boxes and shallow drawn panels — cut on the same 0.001 mm machines that machine our mold plates.
What buyers type when they search this range
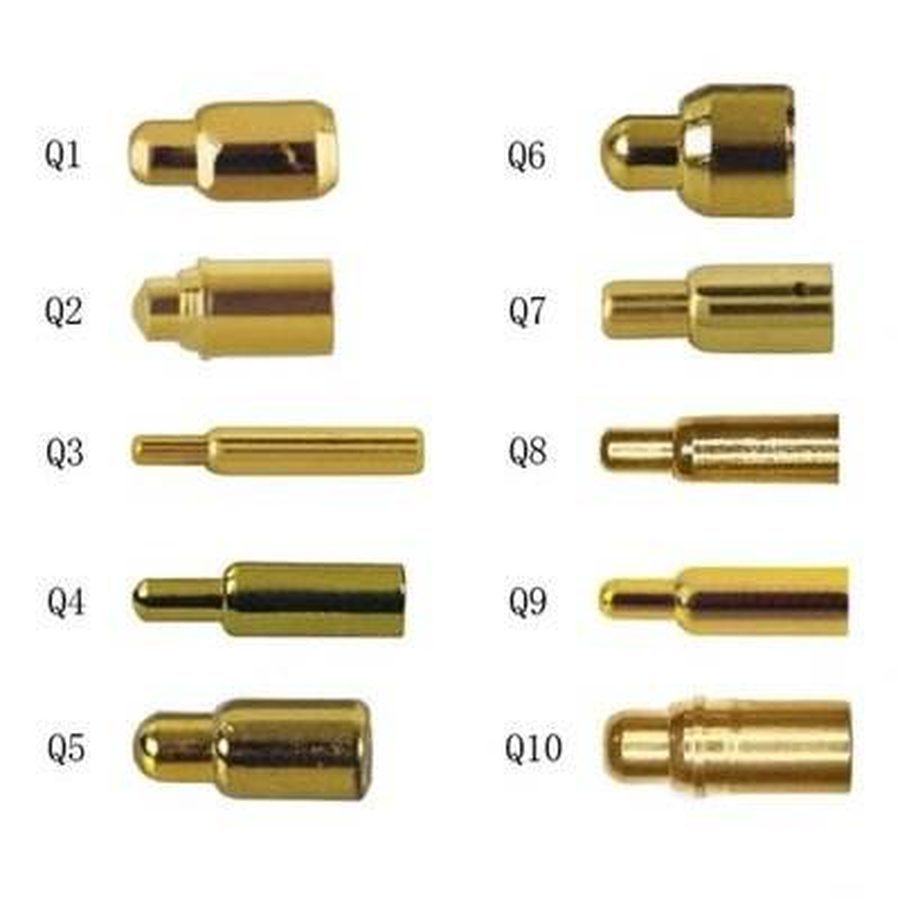
Small turned and milled contacts — pogo pins, terminals and spacers — machined to the same ±0.01 mm the toolroom works to.
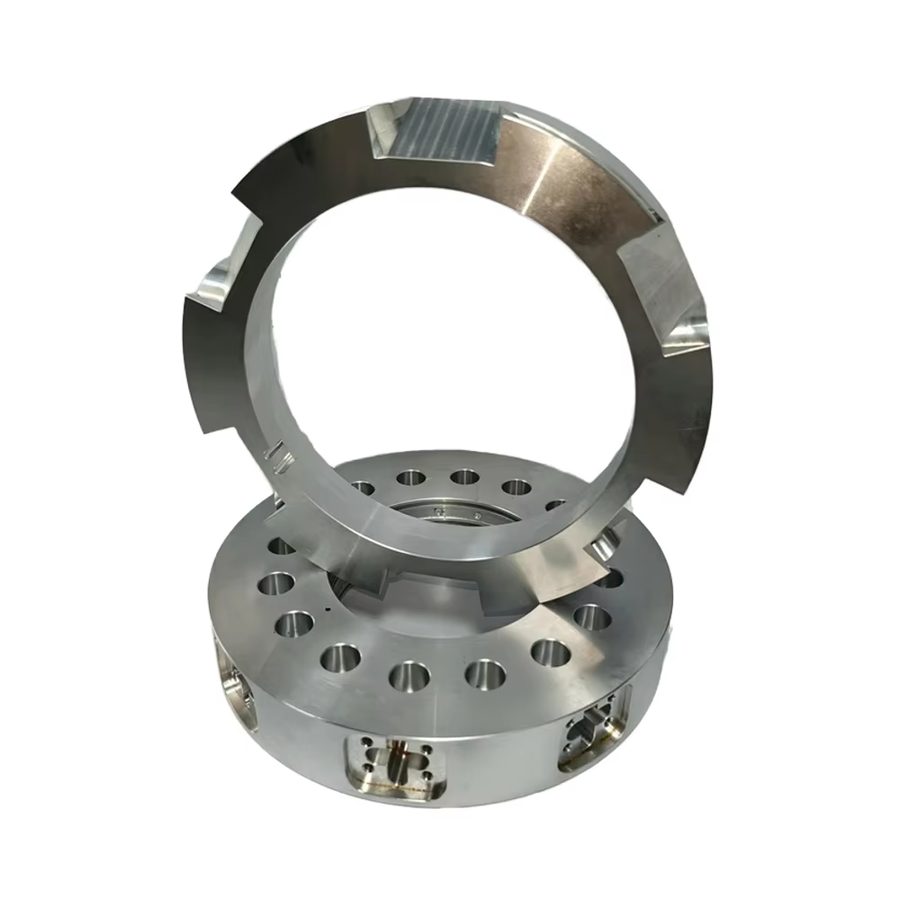
Rings, collars and spacer sets milled and turned from stainless steel and aluminium, with bores and faces held to a common datum.
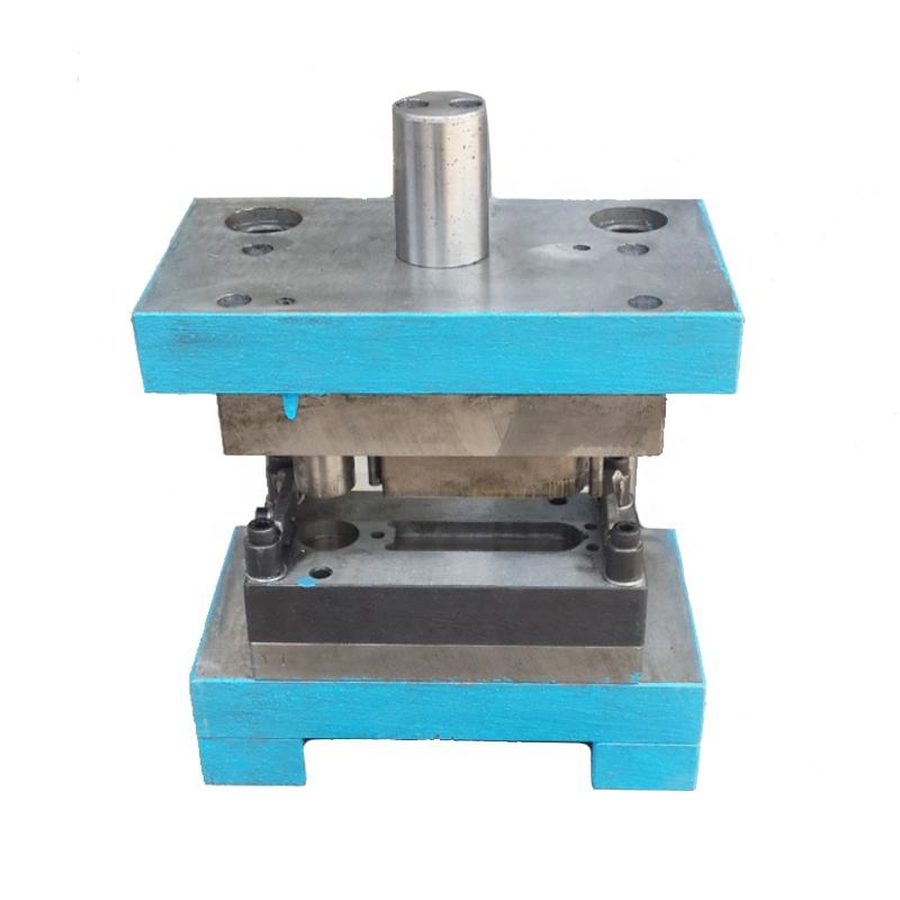
A single-station stamping die for tinplate boxes and shallow drawn panels — built, tried and corrected in the same toolroom as our injection molds.
Category 05 · Precision injection parts
Tight-tolerance molded components in engineering resins: device housings, technical parts, over-molded assemblies and optical-grade transparent parts, molded on the same 30 presses that run the tool trial.
What buyers type when they search this range
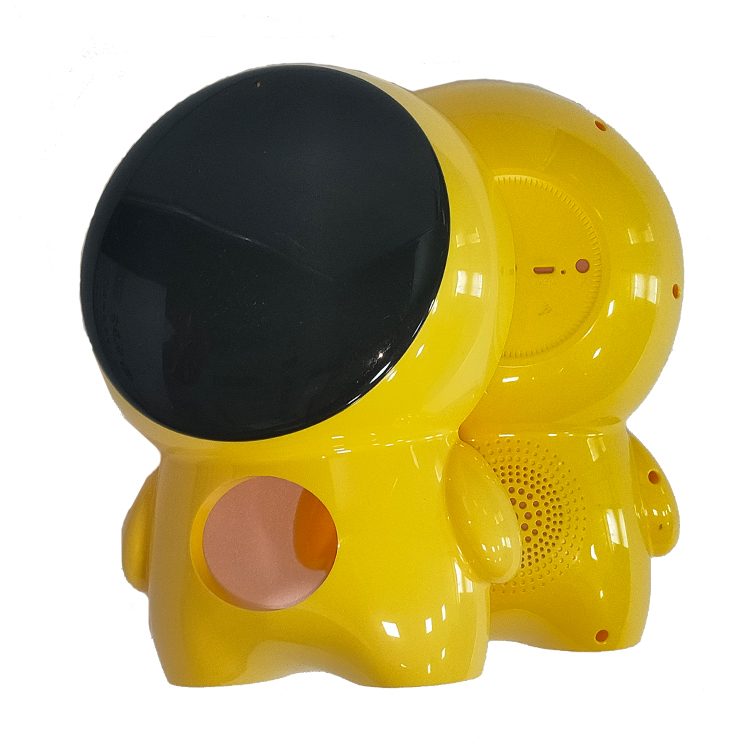
A molded shell with a screen aperture, speaker details and assembly features — tooling, molding and fit handled as one project.
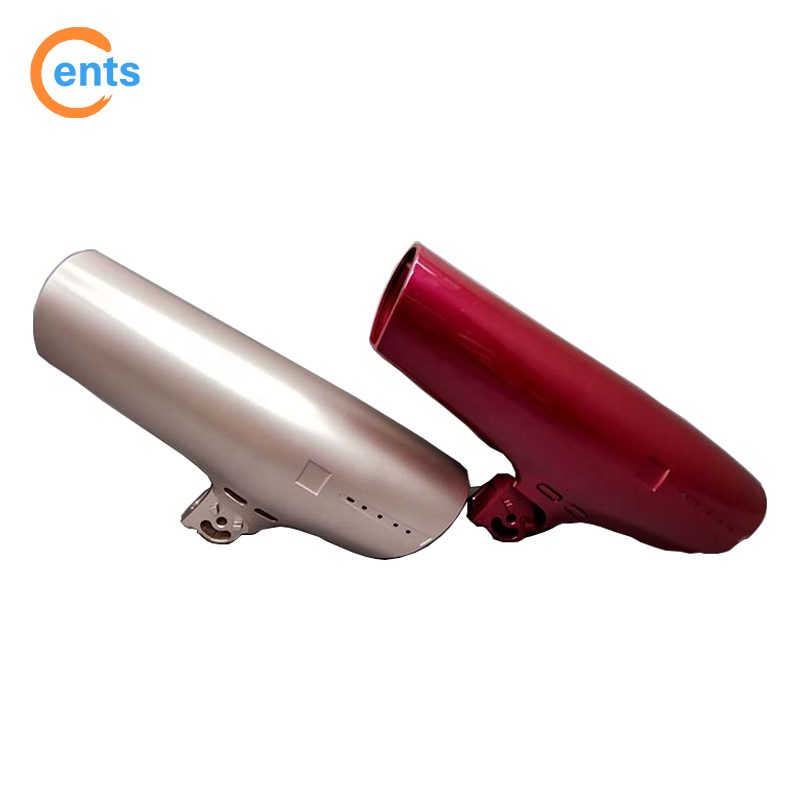
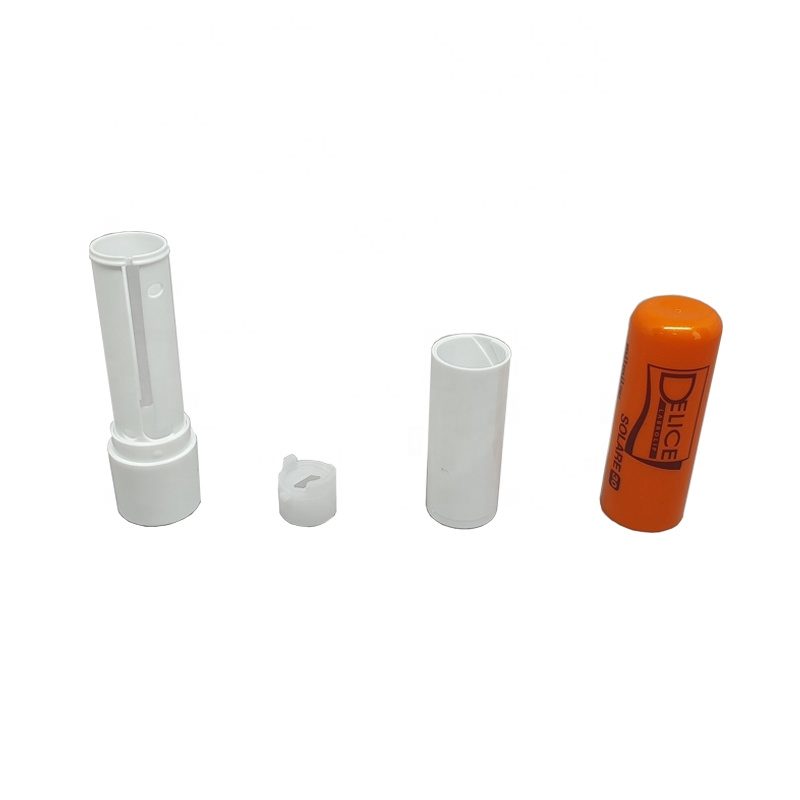
Tube, cap and mechanism components molded to the fit that makes a cosmetic package feel expensive in the hand.
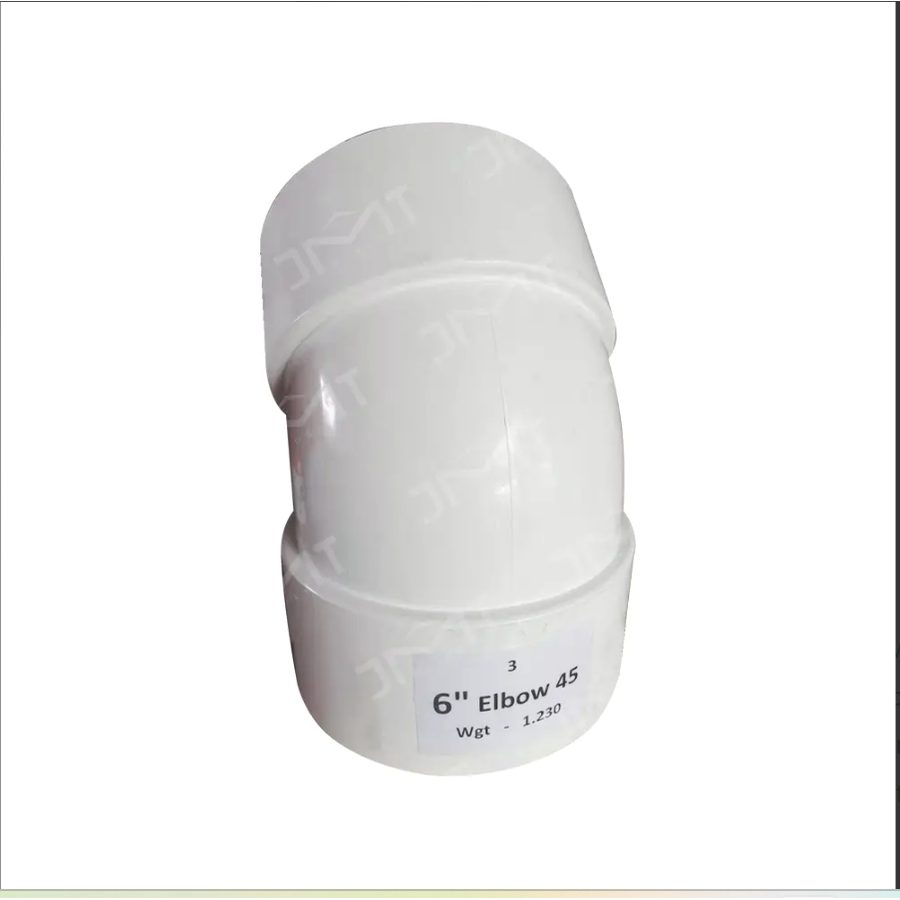
A pipe fitting molded with internal cores and a sealing socket — dimensional accuracy matters far more than appearance.
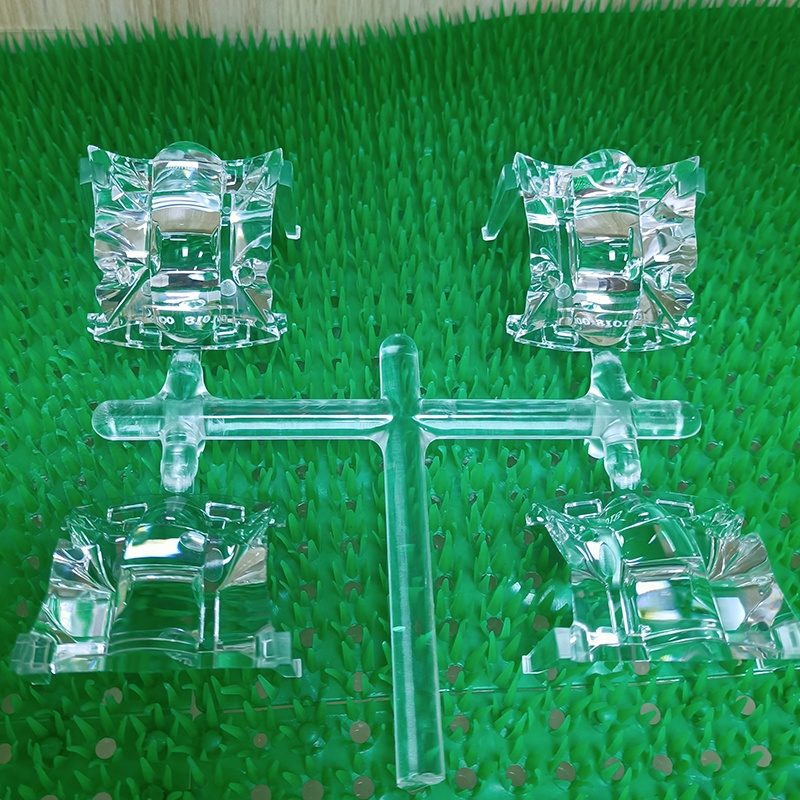
Clear parts to optical standards — the tooling and steel choice do most of the work.
Structural parts in glass-filled polyamide — high strength, abrasive melt, and a mold built for the wear.
Electronics enclosures where venting, wall thickness and appearance all land in the same part.
A sample spread of small precision parts — gears, clips, terminals — across materials and tolerances.
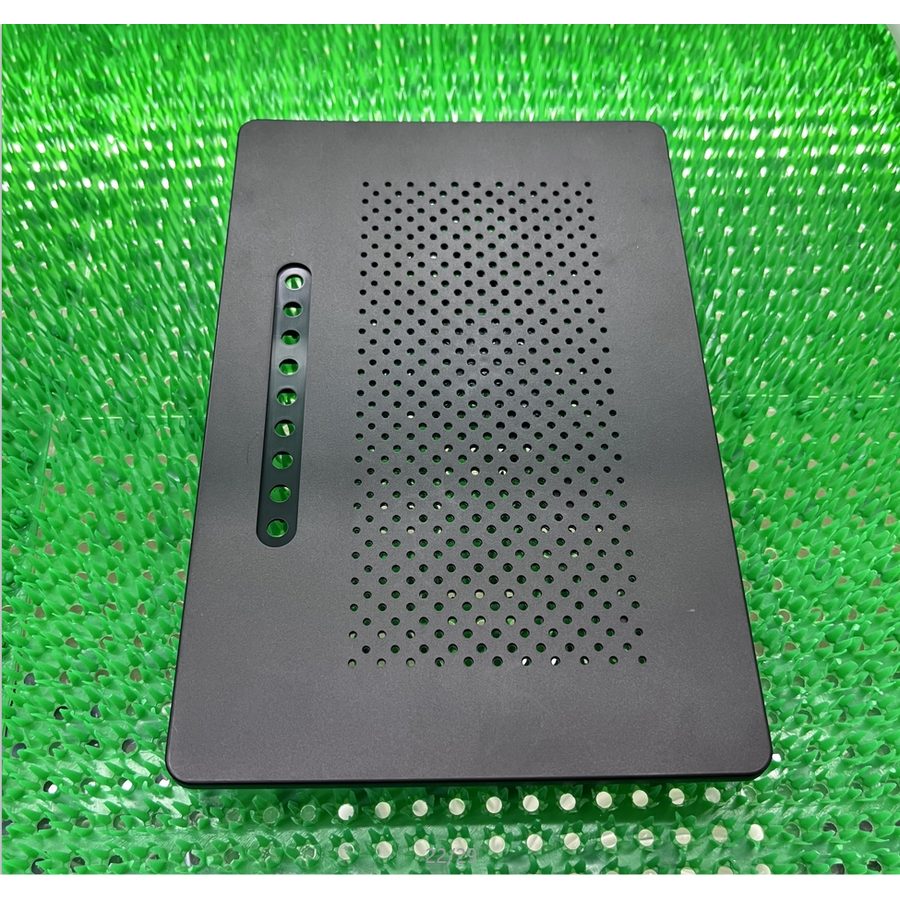
Speaker grilles and vented panels with hundreds of holes — core-pin tooling and flow balance in one part.
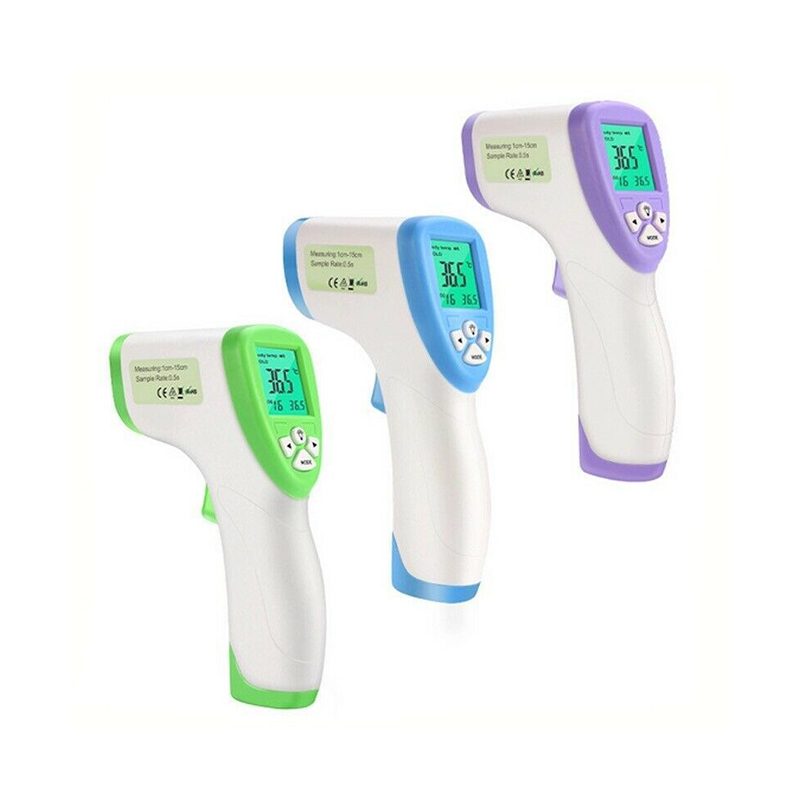
Enclosures for handheld instruments — ergonomics, internal fits and a surface that survives constant handling.
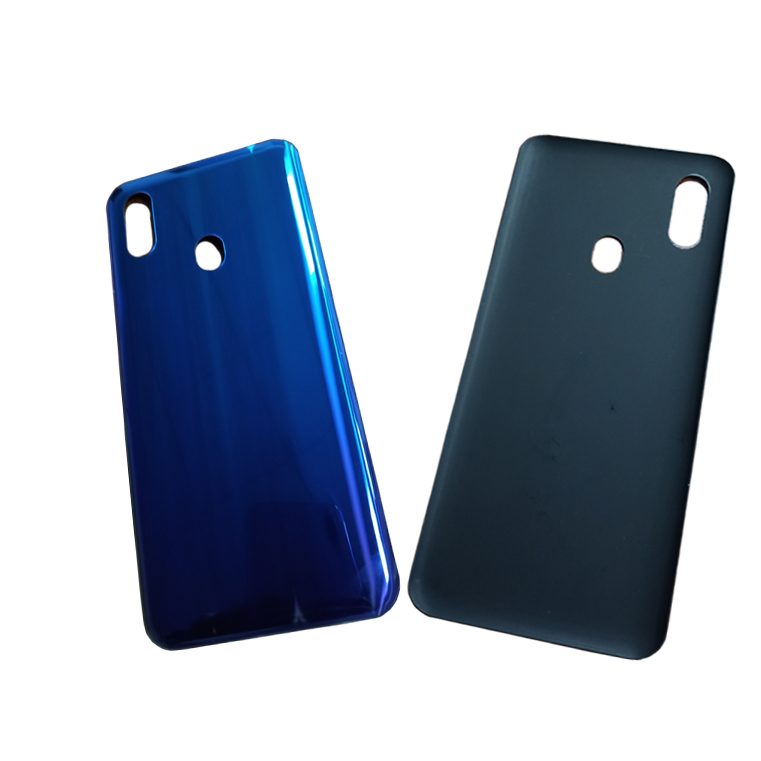
Slim protective covers with a durable surface and precise cut-outs for cameras, sensors and connectors.
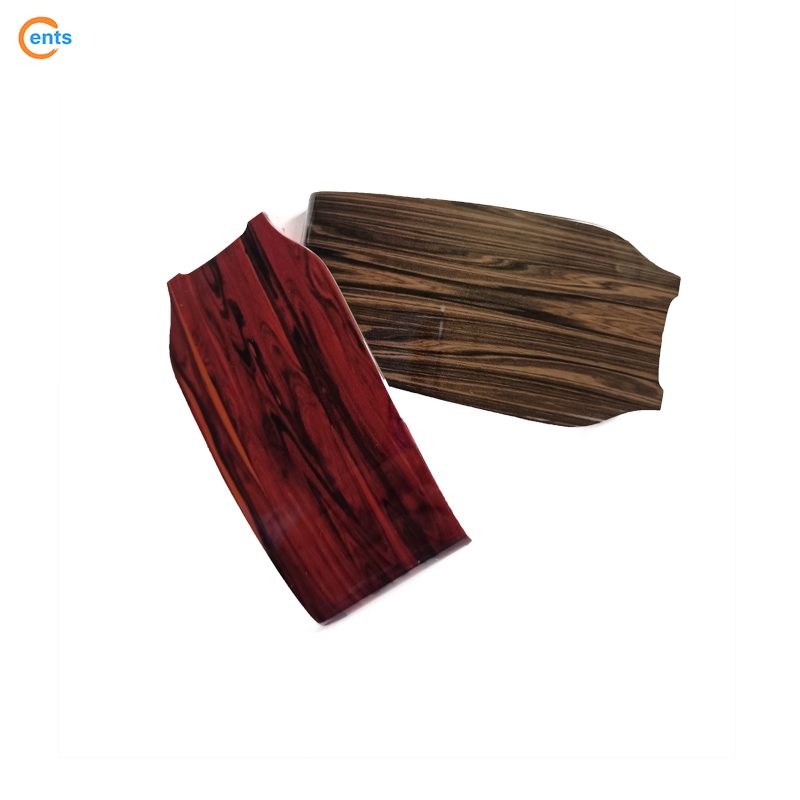
Wood and stone effects produced by the mold surface rather than by a coating — durable in wet and high-touch applications.
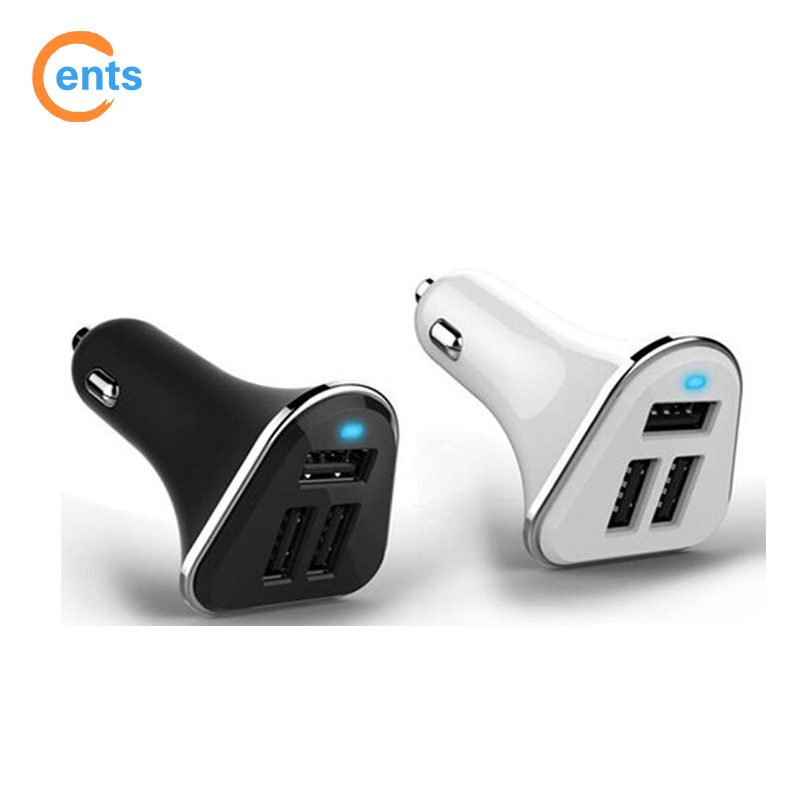
Compact two-part enclosures for vehicle chargers, where the metal contacts and the housing must fit first time.
Functional automotive parts — clips, levers, brackets — molded to repeatable tolerances with documented material traceability.
Large appliance housings that must be watertight at the seams and rigid enough not to flex when filled.
What you get with every tool
Whatever the construction, the same engineering and documentation standards apply.
| Mold construction | Two-plate, three-plate, hot runner, stack or family — specified per part |
| Cavity count | Single or multi-cavity, sized to annual volume, cycle time and press tonnage |
| Mold steels | P20, 718H, NAK80, S136, hardened H13 / SKD61 cores |
| Mold work tolerance | ±0.01 mm |
| Machine accuracy | Down to 0.001 mm (Yasoda, OKUMA, GF, Makino) |
| Runner | Cold runner, hot runner or valve gate |
| Surface finish | SPI A1–D3, bead blast, leather grain or your texture |
| Cooling | Machined circuits; baffles or bubblers where geometry requires |
| Ejection | Pins, sleeves, stripper plate, lifters, unscrewing or collapsible core |
| Verification | Swiss Hexagon CMM and Zeiss Contura; dimensional report at T1 |
| Molding | 30 presses from 20T to 300T, in the same building |
| Documentation | 2D/3D drawings, steel and component certificates, parameter sheet, spare parts |
| Lead time | Typically 15–30 days of machining after design approval |
| Tool ownership | Yours — the tool is designed to be transferable |
Values above are our standard capability for this class of tool, not fixed figures for a specific project. Cavity count, steel grade, runner type and finish are agreed with you on the design approval sheet before any steel is cut.
Your part, not a catalogue item
Include the resin, the annual volume and the market you sell into. You receive a mold price, a molded-part price, a cycle estimate and a written DFM opinion — usually within 1–2 business days.